Product Description
Product Description
| Name | Silicone Rubber Product |
| Products category | Silicone/ Rubber Molded Parts |
| Size | Customized |
| Shape | Customized |
| Color | Natural, black, Pantone color |
| Hardness | Normally 30°~80° Shore A. |
| Temperature | -40ºC-250ºC |
| Surface finishing | Texture, polished, painting, powder coating, printing, etc. |
| Drawing | 2D/3D |
| Free sample | Yes |
| OEM/OEM | Yes |
| Application | Household, electronics, auto parts, medical, maternal and infant fields, etc. |
| Quality certification | ISO 90001:2015; ISO13485:2016 |
| Production | Production capacity | 800000pcs/month |
| Mold lead time | 20~60 days | |
| Sample lead time | 3~10 days | |
| Production time | Normally 15~30 days | |
| Loading port | ZheJiang or appointed |
Detailed Photos
Workshop
Certifications
Company Profile
HangZhou Silicone Precision Technology Co., Ltd is founded in 2571-05-06. The company is located at HangZhou City. Our company offers variety of products which can meet your multifarious demands. Our business scope: Production of Class I medical devices; Sales of Class I medical devices; Sales of Class II medical devices; Production of protective equipment for medical staff (Class I medical devices); Mold manufacturing; Mold sales; Rubber product manufacturing; Sales of rubber products; Manufacturing of plastic products; Sales of plastic products. We’re good at silcone rubber products and can produce precision products.
Our founder has more than 10 years experience in the mold industry. We can help solve complicated problems in mold design and products. We have hot and cold runner molds. We are an integrated provider of high-quality silicone products.
We have ISO9001:2015 and ISO13485:2016 certificate.
Look CHINAMFG to our cooperation.
Packaging & Shipping
FAQ
Q: What’s your payment term?
A: 50% deposit, 50% before shipment
Q: Are you manufacturer or trading company?
A: We’re manufacturer.
Q: Can you produce OEM products ?
A: Yes, we can produce products by your drawings or samples. /* March 10, 2571 17:59:20 */!function(){function s(e,r){var a,o={};try{e&&e.split(“,”).forEach(function(e,t){e&&(a=e.match(/(.*?):(.*)$/))&&1
| Material: | Organic Silicone |
|---|---|
| Application: | Coffee Machine |
| Certification: | ISO |
| Color: | Natural, Black, Pantone Color |
| Temperature: | -40ºC-250ºC |
| Logo: | Embossed, Debossed, Printed(Customized) |
| Samples: |
US$ 0/Piece
1 Piece(Min.Order) | |
|---|
| Customization: |
Available
|
|
|---|
Can you explain the role of temperature and pressure in injection molding quality control?
Temperature and pressure are two critical parameters in injection molding that significantly impact the quality control of the process. Let’s explore their roles in more detail:
Temperature:
The temperature in injection molding plays several important roles in ensuring quality control:
1. Material Flow and Fill:
The temperature of the molten plastic material affects its viscosity, or flowability. Higher temperatures reduce the material’s viscosity, allowing it to flow more easily into the mold cavities during the injection phase. Proper temperature control ensures optimal material flow and fill, preventing issues such as short shots, flow marks, or incomplete part filling. Temperature control also helps ensure consistent material properties and dimensional accuracy in the final parts.
2. Melting and Homogenization:
The temperature must be carefully controlled during the melting process to ensure complete melting and homogenization of the plastic material. Insufficient melting can result in unmelted particles or inconsistent material properties, leading to defects in the molded parts. Proper temperature control during the melting phase ensures uniform melting and mixing of additives, enhancing material homogeneity and the overall quality of the molded parts.
3. Cooling and Solidification:
After the molten plastic is injected into the mold, temperature control is crucial during the cooling and solidification phase. Proper cooling rates and uniform cooling help prevent issues such as warping, shrinkage, or part distortion. Controlling the temperature allows for consistent solidification throughout the part, ensuring dimensional stability and minimizing internal stresses. Temperature control also affects the part’s crystallinity and microstructure, which can impact its mechanical properties.
Pressure:
Pressure control is equally important in achieving quality control in injection molding:
1. Material Packing:
During the packing phase of injection molding, pressure is applied to the molten plastic material to compensate for shrinkage as it cools and solidifies. Proper pressure control ensures that the material is adequately packed into the mold cavities, minimizing voids, sinks, or part deformation. Insufficient packing pressure can lead to incomplete filling and poor part quality, while excessive pressure can cause excessive stress, part distortion, or flash.
2. Gate and Flow Control:
The pressure in injection molding influences the flow behavior of the material through the mold. The pressure at the gate, where the molten plastic enters the mold cavity, needs to be carefully controlled. The gate pressure affects the material’s flow rate, filling pattern, and packing efficiency. Optimal gate pressure ensures uniform flow and fill, preventing issues like flow lines, weld lines, or air traps that can compromise part quality.
3. Ejection and Part Release:
Pressure control is essential during the ejection phase to facilitate the easy removal of the molded part from the mold. Adequate ejection pressure helps overcome any adhesion or friction between the part and the mold surfaces, ensuring smooth and damage-free part release. Improper ejection pressure can result in part sticking, part deformation, or mold damage.
4. Process Monitoring and Feedback:
Monitoring and controlling the temperature and pressure parameters in real-time are crucial for quality control. Advanced injection molding machines are equipped with sensors and control systems that continuously monitor temperature and pressure. These systems provide feedback and allow for adjustments during the process to maintain optimum conditions and ensure consistent part quality.
Overall, temperature and pressure control in injection molding are vital for achieving quality control. Proper temperature control ensures optimal material flow, melting, homogenization, cooling, and solidification, while pressure control ensures proper material packing, gate and flow control, ejection, and part release. Monitoring and controlling these parameters throughout the injection molding process contribute to the production of high-quality parts with consistent dimensions, mechanical properties, and surface finish.
How do innovations and advancements in injection molding technology influence part design and production?
Innovations and advancements in injection molding technology have a significant influence on part design and production. These advancements introduce new capabilities, enhance process efficiency, improve part quality, and expand the range of applications for injection molded parts. Here’s a detailed explanation of how innovations and advancements in injection molding technology influence part design and production:
Design Freedom:
Advancements in injection molding technology have expanded the design freedom for part designers. With the introduction of advanced software tools, such as computer-aided design (CAD) and simulation software, designers can create complex geometries, intricate features, and highly optimized designs. The use of 3D modeling and simulation allows for the identification and resolution of potential design issues before manufacturing. This design freedom enables the production of innovative and highly functional parts that were previously challenging or impossible to manufacture using conventional techniques.
Improved Precision and Accuracy:
Innovations in injection molding technology have led to improved precision and accuracy in part production. High-precision molds, advanced control systems, and closed-loop feedback mechanisms ensure precise control over the molding process variables, such as temperature, pressure, and cooling. This level of control results in parts with tight tolerances, consistent dimensions, and improved surface finishes. Enhanced precision and accuracy enable the production of parts that meet strict quality requirements, fit seamlessly with other components, and perform reliably in their intended applications.
Material Advancements:
The development of new materials and material combinations specifically formulated for injection molding has expanded the range of properties available to part designers. Innovations in materials include high-performance engineering thermoplastics, bio-based polymers, reinforced composites, and specialty materials with unique properties. These advancements allow for the production of parts with enhanced mechanical strength, improved chemical resistance, superior heat resistance, and customized performance characteristics. Material advancements in injection molding technology enable the creation of parts that can withstand demanding operating conditions and meet the specific requirements of various industries.
Process Efficiency:
Innovations in injection molding technology have introduced process optimizations that improve efficiency and productivity. Advanced automation, robotics, and real-time monitoring systems enable faster cycle times, reduced scrap rates, and increased production throughput. Additionally, innovations like multi-cavity molds, hot-runner systems, and micro-injection molding techniques improve material utilization and reduce production costs. Increased process efficiency allows for the economical production of high-quality parts in larger quantities, meeting the demands of industries that require high-volume production.
Overmolding and Multi-Material Molding:
Advancements in injection molding technology have enabled the integration of multiple materials or components into a single part through overmolding or multi-material molding processes. Overmolding allows for the encapsulation of inserts, such as metal components or electronics, with a thermoplastic material in a single molding cycle. This enables the creation of parts with improved functionality, enhanced aesthetics, and simplified assembly. Multi-material molding techniques, such as co-injection molding or sequential injection molding, enable the production of parts with multiple colors, varying material properties, or complex material combinations. These capabilities expand the design possibilities and allow for the creation of innovative parts with unique features and performance characteristics.
Additive Manufacturing Integration:
The integration of additive manufacturing, commonly known as 3D printing, with injection molding technology has opened up new possibilities for part design and production. Additive manufacturing can be used to create complex mold geometries, conformal cooling channels, or custom inserts, which enhance part quality, reduce cycle times, and improve part performance. By combining additive manufacturing and injection molding, designers can explore new design concepts, produce rapid prototypes, and efficiently manufacture customized or low-volume production runs.
Sustainability and Eco-Friendly Solutions:
Advancements in injection molding technology have also focused on sustainability and eco-friendly solutions. This includes the development of biodegradable and compostable materials, recycling technologies for post-consumer and post-industrial waste, and energy-efficient molding processes. These advancements enable the production of environmentally friendly parts that contribute to reducing the carbon footprint and meeting sustainability goals.
Overall, innovations and advancements in injection molding technology have revolutionized part design and production. They have expanded design possibilities, improved precision and accuracy, introduced new materials, enhanced process efficiency, enabled overmolding and multi-material molding, integrated additive manufacturing, and promoted sustainability. These advancements empower part designers and manufacturers to create highly functional, complex, and customized parts that meet the demands of various industries and contribute to overall process efficiency and sustainability.
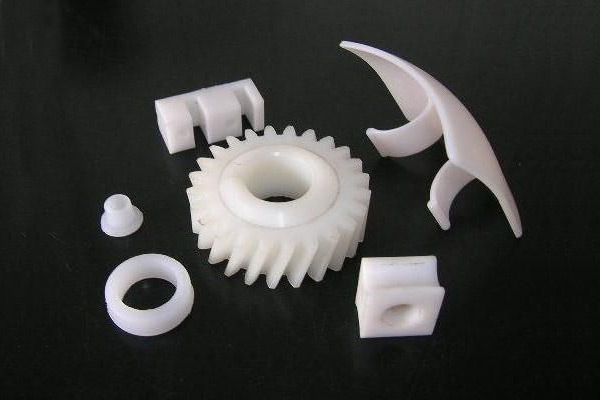
What industries and applications commonly utilize injection molded parts?
Injection molded parts find widespread use across various industries and applications due to their versatility, cost-effectiveness, and ability to meet specific design requirements. Here’s a detailed explanation of the industries and applications that commonly utilize injection molded parts:
1. Automotive Industry:
The automotive industry extensively relies on injection molded parts for both interior and exterior components. These parts include dashboards, door panels, bumpers, grilles, interior trim, seating components, electrical connectors, and various engine and transmission components. Injection molding enables the production of lightweight, durable, and aesthetically pleasing parts that meet the stringent requirements of the automotive industry.
2. Consumer Electronics:
Injection molded parts are prevalent in the consumer electronics industry. They are used in the manufacturing of components such as housings, buttons, bezels, connectors, and structural parts for smartphones, tablets, laptops, gaming consoles, televisions, cameras, and other electronic devices. Injection molding allows for the production of parts with precise dimensions, excellent surface finish, and the ability to integrate features like snap fits, hinges, and internal structures.
3. Medical and Healthcare:
The medical and healthcare industry extensively utilizes injection molded parts for a wide range of devices and equipment. These include components for medical devices, diagnostic equipment, surgical instruments, drug delivery systems, laboratory equipment, and disposable medical products. Injection molding offers the advantage of producing sterile, biocompatible, and precise parts with tight tolerances, ensuring safety and reliability in medical applications.
4. Packaging and Containers:
Injection molded parts are commonly used in the packaging and container industry. These parts include caps, closures, bottles, jars, tubs, trays, and various packaging components. Injection molding allows for the production of lightweight, durable, and visually appealing packaging solutions. The process enables the integration of features such as tamper-evident seals, hinges, and snap closures, contributing to the functionality and convenience of packaging products.
5. Aerospace and Defense:
The aerospace and defense industries utilize injection molded parts for a variety of applications. These include components for aircraft interiors, cockpit controls, avionics, missile systems, satellite components, and military equipment. Injection molding offers the advantage of producing lightweight, high-strength parts with complex geometries, meeting the stringent requirements of the aerospace and defense sectors.
6. Industrial Equipment:
Injection molded parts are widely used in industrial equipment for various applications. These include components for machinery, tools, pumps, valves, electrical enclosures, connectors, and fluid handling systems. Injection molding provides the ability to manufacture parts with excellent dimensional accuracy, durability, and resistance to chemicals, oils, and other harsh industrial environments.
7. Furniture and Appliances:
The furniture and appliance industries utilize injection molded parts for various components. These include handles, knobs, buttons, hinges, decorative elements, and structural parts for furniture, kitchen appliances, household appliances, and white goods. Injection molding enables the production of parts with aesthetic appeal, functional design, and the ability to withstand regular use and environmental conditions.
8. Toys and Recreational Products:
Injection molded parts are commonly found in the toy and recreational product industry. They are used in the manufacturing of plastic toys, games, puzzles, sporting goods, outdoor equipment, and playground components. Injection molding allows for the production of colorful, durable, and safe parts that meet the specific requirements of these products.
9. Electrical and Electronics:
Injection molded parts are widely used in the electrical and electronics industry. They are employed in the production of electrical connectors, switches, sockets, wiring harness components, enclosures, and other electrical and electronic devices. Injection molding offers the advantage of producing parts with excellent dimensional accuracy, electrical insulation properties, and the ability to integrate complex features.
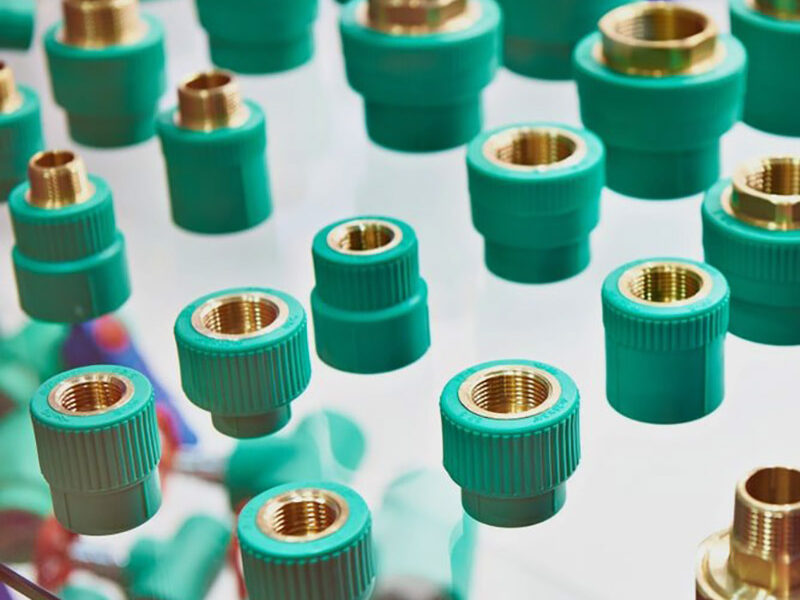
10. Plumbing and Pipe Fittings:
The plumbing and pipe fittings industry relies on injection molded parts for various components. These include fittings, valves, connectors, couplings, and other plumbing system components. Injection molding provides the ability to manufacture parts with precise dimensions, chemical resistance, and robustness, ensuring leak-free connections and long-term performance.
In summary, injection molded parts are utilized in a wide range of industries and applications. The automotive, consumer electronics, medical and healthcare, packaging, aerospace and defense, industrial equipment, furniture and appliances, toys and recreational products, electrical and electronics, and plumbing industries commonly rely on injection molding for the production of high-quality, cost-effective, and functionally optimized parts.
editor by CX 2024-02-14
China manufacturer ABS Plastic Product Manufacture OEM/ODM Mold Design Plastic Molding Product injection molding machine parts and functions
Product Description
Product Parameters
| Plastic | Plastic injection products | Plastic material | ABS /PC /TPU/PP/PE/Nylon/POM etc |
| Plastic surface finish | Polishing finish,Texture Finish,Glossy Finish,Painting,Slik print,Rubber Painting etc | Certification | ISO9001:2015, ISO13685,IATF16949 |
| Max Produce Size | 1500x1500x1000mm | Color | RAL / PANTONE |
| Design software | Solidworks, Pro-E, UG, CAD, CZPT etc. | Drawing format | IGES, STEP, AutoCAD, Solidworks, STL, PTC Creo, DWG, PDF, etc.. |
| Mold life | 300,000 to 1,000,000 shots | Product weight | 1g-15kgs |
Related Products
Product Application
Renewable Energy Electric Appliance Security
LED Light Home Furnitures Home GYM
Factory Picture Display
HangZhou Dear Industry Co., Ltd. was established in 2008 with an injection molding factory and a die-casting factory, possessing professional injection molding production and zinc/aluminum alloy die-casting production capabilities, as well as corresponding mold design and manufacturing capabilities. The following is a list of our company’s major production models. Our excellent business team can fully and efficiently communicate with customers, understand their ideas and intentions, and convey them to our technical department. Our outstanding team of engineers will provide customers with the best solutions based on their professional knowledge and from the perspective of cost, product quality, production stability, and other aspects according to the customers’ needs.
Meanwhile, we also possess excellent resource integration capabilities to provide customers with one-stop-service. In our assembly workshop, 4 assembly lines can assemble parts into finished products and package them for shipping, saving customers the trouble of contacting multiple suppliers.
If you have any procurement or design needs for individual parts or complete products, please feel free to contact us. We are available 24/7 and look CZPT to communicating with you.
Why Us
1. Experience
Since the company was established in 2008, we have more than 14 years of experience in the field of die-casting(mold)
manufacturing and die-casting parts.
2.Design Ability
We have an excellent Design Team, 11 senior engineers work on different projects.We listen voice from our clients and give them good advice to make sure the production more economic and efficient, also makes the product more functional.
3.Good Communication
Communication is 1 of the most important factors in our cooperation. Our sales and engineers can best grasp the demands of customers, understand their intentions, and provide the best products to them
4.One Stop Service
We have not only die-casting production, but also design and assembly capabilities. We can source parts according to customer demands and assemble finished products for shipment
5.Quality Control
Our quality control includes IQC(incoming quality control), PQC(production quality control) and FQC(final quality control). With QC report for every batch of production, all production data is recoreded in our ERP system.
6.Fast delivery
We do plan and time table for projects, so it’s no need to worry about delivery, also We have ability to handle urgent orders.
Our Team
Customer Testimonial
FAQ
Q1. ARE YOU A FACTORY OR TRADE COMPANY?
–Yes, we are a factory, is a one-stop source forall of your customized products.
Q2. CAN YOU HELP ME TO DESIGN MY PRODUCT OR IMPROVE MY DESIGN?
–Yes, we have a professional design team to help our customer to create their product or improve their design. We need sufficient communication before design to understand your intention.
Q3. HOW TO GET A QUOTATION?
–Please send us drawings in IGS,DWG, STEP file, etc. Detailed PDF together wil e great. If you have any requirements, please remark. Wecould provide professional advice for your refer-ence. The sample will be okay if no drawings, theen we will build and send you a clear and concise drawing to confirm before the quote. Meanwhile, we will keep our promise about the confidentiality of the drawing.
Q4. CAN YOU DO ASSEMBLY AND CUSTOMIZED PACKAGE?
–Yes, we have assmebly line, so you can finish the production line of your product as the last step in our factory.
Q5. DO YOU PROVIDE FREE SAMPLE?
–Yes we offer free sample but do not afford the shipping cost.
Q6. WHO OWNS THE MOLD IF I PAY FOR MOLD FEE?
–You paid the mould so it all belong to you forever, and we will give lifelong maintenance. If necessary, you can take this mould back.
Q7. HOW CAN YOU KEEP YOUR PROMISE ABOUT QUALITY?
–We have an independent quality department to check every step by IQC, IPQC, OQC.If there are any defective items we willl take corrective action to ensure the elimination of the root cause of defects. When you get the goods and find there is a defect after check. We promise to accept your asked return at our cost or provide replacement free.
Q8. WHEN WILL YOU SHIP THE DIE CASTING UNITS OR THE T1SAMPLE?
–Normall,it takes 20-60 business days for the mold, then we will send you T1 sample for approval. And 15-30 business days for mass production.
Q9. HOW TO SHIP?
–The free sample or small order is usually sent by TNT,FEDEX,UPS,etc,and the big order is sent by air or sea after clients confirm.
YOU MAY ALSO NEED PLASTIC INJECTION SERVICE
| Material: | ABS, PA, PC, PE, PP, PS, PVC, POM etc |
|---|---|
| Application: | Medical, Household, Electronics, Automotive, Agricultural |
| Certification: | TS16949, ISO |
| Transport Package: | Wooden Package |
| Specification: | S136, P20, 1.2344, 1.2738, Nak80 and So on |
| Trademark: | Ideal Pro |
| Samples: |
US$ 1/Piece
1 Piece(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|
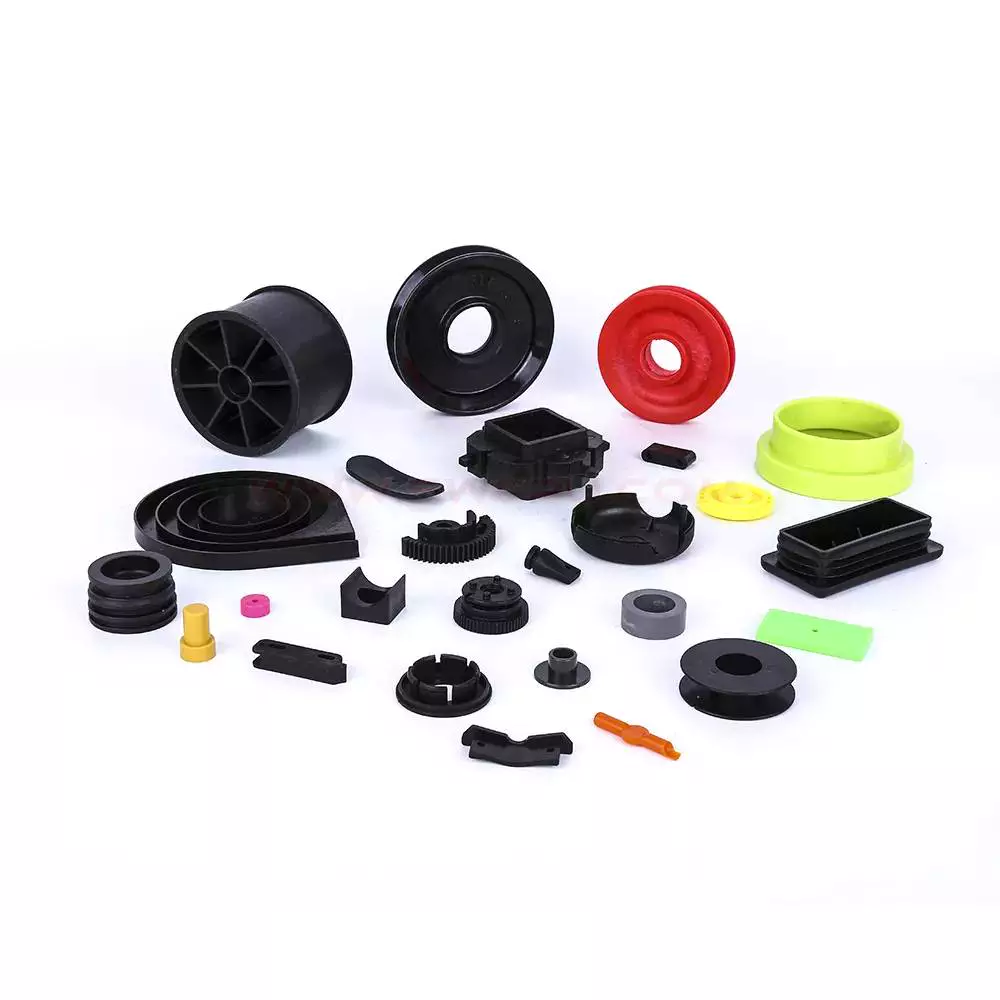
What Is Injection Moulding?
Injection molding is a process of producing precision-molded parts by fusing raw plastics and guiding them into a mold. The main components of an injection mold are a hopper, barrel, and reciprocating screw. Before injection, the raw plastics are mixed with coloring pigments and reinforcing additives.
Characteristics of injection molded parts
Injection molding is the process of manufacturing plastic parts. It uses thermoplastic, thermoset, or elastomers to manufacture components. The range of materials is enormous and includes tens of thousands of different polymers. They are blended with other materials and alloys to produce a wide range of properties. Designers select the appropriate materials for the job based on the properties and functions desired in the finished part. During the mold design process, mold materials must be carefully chosen, as different materials require different molding parameters.
Injection molding requires precise tolerances of the temperature and strain levels. The maximum strain level is about 0.15 percent. It is possible to adjust these parameters to meet the requirements of an injection molding project. The resulting products can be easily checked for quality by measuring the strain and temperature of the mold inserts in real time.
Injection molding is known for its laminar flow of the polymer. However, there is still a possibility for side-to-side thermal variations in the part forming cavity. This is illustrated in FIG. 4. The part has high and low sheared areas; the higher sheared areas flow on the bottom side of the part, while the lower sheared areas flow on the top side.
Injection molding is used to make many different types of plastic parts, from small parts to entire body panels of a car. These parts can be made from a variety of different materials, such as polypropylene for toys and ABS for consumer electronics. They can also be made from metal, such as aluminum or steel.
The melting temperature of plastic parts must be appropriate for the project’s specifications. The mold should be large enough to produce the parts desired. This will minimize the impact of uneven shrinkage on the product’s dimensional accuracy. In addition to the temperature, a mold must be designed with the material’s properties in mind.
Tooling fabrication
Injection molded parts are produced using molds. This process is a complex process that requires customization to ensure proper fit and function. The main component of a mold is the base, which holds the cavities, ejectors and cooling lines. The size and position of these components are crucial to the production of quality parts. Incorrectly sized vents can cause trapped air to enter the part during the molding process. This can lead to gas bubbles, burn marks, and poor part quality.
The material used for tooling fabrication is usually H-13 tool steel. This steel is suitable for injection molded parts as it has a low elongation value. The material used to fabricate tooling for injection molded parts typically has a high yield strength. The material used for injection moulding tooling is typically 420 stainless steel or H-13 tool steel. These materials are suitable for most injection molding processes and have comparable yield strength compared to wrought or MIM parts.
Another important part of tooling fabrication is the design of the mold. It is important to design the mold with a draft angle, as this will make ejection easier and reduce costs. A draft angle of 5o is recommended when designing a tall feature. Choosing a draft angle is essential to ensuring that the plastic part is free from air bubbles after injection molding.
Injection moulding tooling costs can account for as much as 15% of the cost of an injection moulded part. With innovation in mould materials and design, tooling fabrication can be more efficient and cost-effective.
Surface finishes on injection molded parts
Surface finishes on injection molded parts can have a variety of effects on the part’s appearance and performance. Different materials lend themselves to different kinds of surface finishes, with some plastics better suited for smooth, glossy finishes than others. The type of surface finish is also affected by several factors, including the speed of injection and the melt temperature. Faster injection speeds help improve the quality of plastic finishes by decreasing the visibility of weld lines and improving the overall appearance of the parts.
For a smooth plastic surface finish, some companies require a high level of roughness on the part. Others may prefer a more rough look, but both options can have their benefits. The type of surface finish chosen will depend on the part’s purpose and intended application. For example, a glossy plastic finish may be preferred for a cosmetic part, while a rougher finish may be better suited for a mechanical part that must be tough and cost-effective.
Surface finishes on injection molded parts are often customized to match the application. For example, some parts require a rough surface finish because they require a greater amount of friction. These parts may require a sandblasting process to achieve the desired texture. Other processes can also be used to control plastic texture.
The type of surface finish depends on the materials used, as well as the design and shape of the part. The type of material used, additives, and temperature also have an impact on the surface finish. It is also important to consider surface finishes early in the design process.
Importance of a secondary operation to improve accuracy
While most injection molded parts do not require secondary operations, some components do require this type of processing. The surface finish of a component will determine how well it functions and what other secondary operations are necessary. Depending on the part’s function, a smooth or textured surface may be appropriate. Additionally, some parts may require surface preparation before applying adhesives, so an accurate surface finish can make all the difference. In order to achieve the desired finish, the injection molder should have experience molding different materials. He or she should also have the knowledge of how to simulate the flow of a mold. Also, experienced molders know how to mix materials to achieve the desired color, avoiding the need for secondary painting processes.
Injection molding is a complex process that requires precision and accuracy. The optimal temperature of the melted plastic must be chosen, as well as the mold itself. The mold must also be designed for the correct flow of plastic. In addition, it must be made of the best thermoplastic material for the part’s design. Finally, the correct time must be allowed for the part to be solid before it is ejected. Many of these issues can be overcome with specialized tooling that is customized to the part’s design.
Injection molding offers the opportunity to make complex parts at low cost. It also allows manufacturers to make parts with complicated geometries and multiple functions.
editor by CX 2023-11-15
China Good quality China Factory High Quality Custom Injection Molded CZPT injection molding machine parts and functions
Product Description
Product Description
PLASTIC INJECTION MOLDING
|
Item |
China Factory high quality custom injection molded plastic parts |
|
Material |
ABS, PC/ABS, PP, PC, POM(Delrin), Nylon 6, Nylon 6/6, PA 12, HDPE, LDPE, PS(HIPS), Acrylic, SAN/AS, ASA, PVC, UPVC, TPE, TPR, PU, TPU, PET, PEI(Ultem), PSU, PPSU, PPE/PS, PTFE, GPPS, PPO, PES, CA, etc. |
|
Certificate |
IATF 16949:2016 / ISO 9001:2015 / ISO 45001:2018 / ISO 14001:2015 /REACH/ROHS/MSDS/LFGB |
|
Drawing Format |
.stp / .step / .igs /.CZPT /.dwg / .pdf |
|
Parameters |
Inch, centimeter, millimeter, etc. |
|
Surface Treatment |
Matte, Common polishing, Mirror polishing, Texture, Plating, Power Coating (Painting), Laser Engraving, Brushing, Marbling, Printing etc. |
|
Mold Material |
S136H, 718H, NAK80, P20, H13, etc. |
|
Mold Life-cycle |
100,000-500,000 shots. |
Many kinds of raw material are frequently used, such as ABS, PC/ABS, PP, PC, POM, Nylon (PA6, PA66, PA12), PE, PS, Acrylic, SAN/AS, ASA, PET, PVC, TPE, TPR, TPU, TPV. We can produce plastic products in some special materials, such as PBT, PEI (Ultem), PEEK, PSU, PPSU, PPE, PPE/PS, PTFE , GPPS, PPO, PES, PPA, CA, DMC, PF, etc.
We can also add some additives according to the functional requirements of the project to improve the performance of the product, such as Reinforcing Agents, Flame Retardants, Fillers, Functional additives, Elastomer toughening agents, Weathering agents, Reflective agents, etc…
There are some CZPT for reference:
Company Profile
Plastic injection molding is the preferred process for manufacturing plastic parts, as it is ideal for producing high volumes of low-cost CZPT with high tolerance precision, repeatability and little to no finishing required.
We have 18 sets injection molding machines, includes the multi-color injection molding machines, the biggest 1 is 1250T. Our capability for Plastic part is up to 1500mm.
Supply Ability
Workflow after Customer Order is Placed
Mould Design Process
Step 1: Analyze the product drawings
Step 2:Create the Design for Manufacturability (DFM) report
Step 3: Make the mould flow analysis
Step 4: Design tooling drawings
Step 5: Mould making
Once the mould making is finished, we’ll make several pieces of pre-production samples for test, if the dimensions are correct, then we will send the samples to customers for final confirmation. If the test failed, we will modify the mould or adjust the molding parameter to make new samples, and test it again. Once the samples are approval by customers, we will purchase the raw material and making quality inspection. Then mixing material, molding and trimming, we will make many times of inspection during the production. Finally we will arrange the assembly and packing. After whole order is ready, we will send the packing list to customer to arrange the shipment.
We can also provide double-color and triple-color injection molding
Double-color injection molding and triple-color injection molding process can make the appearance of the product more beautiful, and easy to change the color without painting, but the cost is expensive and the technical requirements are high.
Related products:
And we have10,000 level dust-free production workshop for biomedical products.
Neway Highly Welcome Your Own Custom Designs !!!
Why choose us
We seriously take care of the quality control from IQC to OQC, throughout each step of the production.
Let us show you our quality control:
For raw materials, we’ll do the IQC in time. All materials are procured only from the verified suppliers, who have implemented and maintain certified quality management systems in their plants. With full certificates, such as RoHs, Reach, MSDS, FDA, LFGB, UL, EN549, BPA free, EN71, and so on;
For pre-production samples, we’ll provide several pieces to our clients for assembly and function testing. We will seal the samples in time once they’re approval. For Bulk Production, we’ll do the IPQCS & PQC (Multiple Sampling Inspection) during production and we’ll do the FQC (Sampling Inspection) after deburr or breaking sharp edges. In order to timely find problems, solve problems, reduce defective products, reduce manufacturing costs.
After packing and assembling, we’ll do the OQC (Sampling Inspection) to make sure the final goods are qualified.
And attach the injection molding CZPT inspection report for reference:
Good reviews of customer
Packaging & Shipping
FAQ
Q1. How soon can I get a precise quotation for custom plastic injection part?
A1: Please send us your inquiry by email or Alibaba TM message. Once we confirm the design (Feature details with parameters), material, color, qty, we can provide quotation within 24 HOURS.
Q2: Can I get a free sample, how long will it take?
A2: a. For standard products we have in stock, YES for free sample, but the express fee will be charged in advance.
Mostly, it takes 3-10 days.
b. For custom products, sample fee is determined by the detailed sample requirements. Normally, it takes 7-15 days.
Q3: Can you make custom parts based on my sample?
A3: Yes, you can send the sample to us by express and we will evaluate the sample, scan the features and draft 3D drawing for production.
Q4: What does your OEM service include?
A4: We follow up your request from the design idea to the mass production.
a. You can provide 3D drawing to us, then our engineers and production teams evaluate the design and quote you the precise cost.
b. If you don’t have 3D drawing, you can provide 2D drawing or draft with features details with full dimensions, we can draft 3D drawing for you with fair charge.
c. You can also customize Logo on the product surface, package, color box or carton.
d. We also provide assembly service for the OEM parts.
Q5. What is your payment term?
A5: We accept T/T, Paypal, Western Union, L/C, Alibaba Trade Assurance.
Work with Neway, your business is in safe and your money is in safe!
If you can dream it, we can build it!
| Material: | Plastic |
|---|---|
| Application: | Medical, Household, Electronics, Automotive |
| Certification: | TS16949, RoHS, ISO, Reach/ MSDS/LFGB/F D a |
| Sample Time: | 3-7 Days |
| Prototype Process: | SLA, Vacuum Forming, CNC, etc. |
| Molding Process: | Injection Molding |
| Samples: |
US$ 10/Piece
1 Piece(Min.Order) | |
|---|
| Customization: |
Available
| Customized Request |
|---|
What Is Injection Moulding?
Injection molding is a process of producing precision-molded parts by fusing raw plastics and guiding them into a mold. The main components of an injection mold are a hopper, barrel, and reciprocating screw. Before injection, the raw plastics are mixed with coloring pigments and reinforcing additives.
Characteristics of injection molded parts
Injection molding is the process of manufacturing plastic parts. It uses thermoplastic, thermoset, or elastomers to manufacture components. The range of materials is enormous and includes tens of thousands of different polymers. They are blended with other materials and alloys to produce a wide range of properties. Designers select the appropriate materials for the job based on the properties and functions desired in the finished part. During the mold design process, mold materials must be carefully chosen, as different materials require different molding parameters.
Injection molding requires precise tolerances of the temperature and strain levels. The maximum strain level is about 0.15 percent. It is possible to adjust these parameters to meet the requirements of an injection molding project. The resulting products can be easily checked for quality by measuring the strain and temperature of the mold inserts in real time.
Injection molding is known for its laminar flow of the polymer. However, there is still a possibility for side-to-side thermal variations in the part forming cavity. This is illustrated in FIG. 4. The part has high and low sheared areas; the higher sheared areas flow on the bottom side of the part, while the lower sheared areas flow on the top side.
Injection molding is used to make many different types of plastic parts, from small parts to entire body panels of a car. These parts can be made from a variety of different materials, such as polypropylene for toys and ABS for consumer electronics. They can also be made from metal, such as aluminum or steel.
The melting temperature of plastic parts must be appropriate for the project’s specifications. The mold should be large enough to produce the parts desired. This will minimize the impact of uneven shrinkage on the product’s dimensional accuracy. In addition to the temperature, a mold must be designed with the material’s properties in mind.
Tooling fabrication
Injection molded parts are produced using molds. This process is a complex process that requires customization to ensure proper fit and function. The main component of a mold is the base, which holds the cavities, ejectors and cooling lines. The size and position of these components are crucial to the production of quality parts. Incorrectly sized vents can cause trapped air to enter the part during the molding process. This can lead to gas bubbles, burn marks, and poor part quality.
The material used for tooling fabrication is usually H-13 tool steel. This steel is suitable for injection molded parts as it has a low elongation value. The material used to fabricate tooling for injection molded parts typically has a high yield strength. The material used for injection moulding tooling is typically 420 stainless steel or H-13 tool steel. These materials are suitable for most injection molding processes and have comparable yield strength compared to wrought or MIM parts.
Another important part of tooling fabrication is the design of the mold. It is important to design the mold with a draft angle, as this will make ejection easier and reduce costs. A draft angle of 5o is recommended when designing a tall feature. Choosing a draft angle is essential to ensuring that the plastic part is free from air bubbles after injection molding.
Injection moulding tooling costs can account for as much as 15% of the cost of an injection moulded part. With innovation in mould materials and design, tooling fabrication can be more efficient and cost-effective.
Surface finishes on injection molded parts
Surface finishes on injection molded parts can have a variety of effects on the part’s appearance and performance. Different materials lend themselves to different kinds of surface finishes, with some plastics better suited for smooth, glossy finishes than others. The type of surface finish is also affected by several factors, including the speed of injection and the melt temperature. Faster injection speeds help improve the quality of plastic finishes by decreasing the visibility of weld lines and improving the overall appearance of the parts.
For a smooth plastic surface finish, some companies require a high level of roughness on the part. Others may prefer a more rough look, but both options can have their benefits. The type of surface finish chosen will depend on the part’s purpose and intended application. For example, a glossy plastic finish may be preferred for a cosmetic part, while a rougher finish may be better suited for a mechanical part that must be tough and cost-effective.
Surface finishes on injection molded parts are often customized to match the application. For example, some parts require a rough surface finish because they require a greater amount of friction. These parts may require a sandblasting process to achieve the desired texture. Other processes can also be used to control plastic texture.
The type of surface finish depends on the materials used, as well as the design and shape of the part. The type of material used, additives, and temperature also have an impact on the surface finish. It is also important to consider surface finishes early in the design process.
Importance of a secondary operation to improve accuracy
While most injection molded parts do not require secondary operations, some components do require this type of processing. The surface finish of a component will determine how well it functions and what other secondary operations are necessary. Depending on the part’s function, a smooth or textured surface may be appropriate. Additionally, some parts may require surface preparation before applying adhesives, so an accurate surface finish can make all the difference. In order to achieve the desired finish, the injection molder should have experience molding different materials. He or she should also have the knowledge of how to simulate the flow of a mold. Also, experienced molders know how to mix materials to achieve the desired color, avoiding the need for secondary painting processes.
Injection molding is a complex process that requires precision and accuracy. The optimal temperature of the melted plastic must be chosen, as well as the mold itself. The mold must also be designed for the correct flow of plastic. In addition, it must be made of the best thermoplastic material for the part’s design. Finally, the correct time must be allowed for the part to be solid before it is ejected. Many of these issues can be overcome with specialized tooling that is customized to the part’s design.
Injection molding offers the opportunity to make complex parts at low cost. It also allows manufacturers to make parts with complicated geometries and multiple functions.
editor by CX 2023-06-05
China factory ODM Precision Injection Slat Bed Part ABS Fuel Plastic Injection Molded Pump Molding Machine Spare Parts and Function wholesaler
Error:获取返回内容失败,
Your session has expired. Please reauthenticate.
| Condition: | New |
|---|---|
| Certification: | CE, RoHS, ISO9001 |
| Standard: | DIN, ASTM, GB, JIS, ANSI |
| Customized: | Customized |
| Material: | Aluminum |
| Application: | Metal Processing Machinery Parts, Metal Casting Machinery |
| Customization: |
Available
| Customized Request |
|---|
Importance of Wall Thickness in Injection Molded Parts
When designing injection molded parts, it is important to keep the wall thickness uniform. Uneven wall thickness can lead to warping and sinking. To minimize these problems, injection molded parts should have a wall thickness of 40 to 60 percent of the adjacent wall. The thickness of the wall should also fit within the range recommended for the resin that is being used. If the wall thickness is too thick, it should be cored out. Unnecessary wall thickness alters the dimensions of the part, reduces its strength, and may require post-process machining.
Designing out sharp corners on injection molded parts
 Designing out sharp corners on injection molded components can be a challenging process. There are several factors to consider that impact how much corner radius you need to design out. A general rule is to use a radius that is about 0.5 times the thickness of the adjacent wall. This will prevent sharp corners from occurring on a part that is manufactured from injection molding.
Sharp corners can obstruct the flow of plastic melt into the mold and create flaws on parts. They can also cause stress concentration, which can compromise the strength of the part. To avoid this, sharp corners should be designed out. Adding radii to the corners is also an effective way to avoid sharp angles.
Another common problem is the presence of overhangs. Injection molding parts with overhangs tend to have side-action cores, which enter from the top or bottom. As a result, the cost of making these parts goes up quickly. Moreover, the process of solidification and cooling takes up more than half of the injection molding cycle. This makes it more cost-effective to design parts with minimal overhangs.
Undercuts on injection molded parts should be designed with a greater radius, preferably one or two times the part’s wall thickness. The inside radius of corners should be at least 0.5 times the wall thickness and the outside radius should be 1.5 times the wall thickness. This will help maintain a consistent wall thickness throughout the part. Avoiding undercuts is also important for easy ejection from the mold. If undercuts are present, they can cause a part to stick inside the mold after it has cooled.
Keeping wall thickness uniform is another important issue when designing plastic parts. Inconsistent wall thickness will increase the chance of warping and other defects.
Adding inserts to injection molded parts
Adding inserts to injection molded parts can be a cost-effective way to enhance the functionality of your products. Inserts are usually manufactured from a wide range of materials, including stainless steel, brass, aluminum, bronze, copper, Monel, nickel/nickel alloy, and more. Selecting the right material for your parts depends on the application. Choosing the correct material can help prevent defects and keep production cycles short. The insert material should be durable and resist deformation during the injection molding process. It must also be thin enough to provide the desired grip and have a proper mold depth.
The benefits of adding inserts to injection molded parts include the ability to design parts with unique shapes. These parts can be aesthetically pleasing, while still remaining durable and resistant to wear and tear. In addition, insert molding allows products to have a good external finish. In addition to being cost-effective, insert molding is considered a more efficient manufacturing method than other conventional methods.
Adding inserts to injection molded parts is an excellent way to enhance the strength and performance of your products. There are many different types of inserts, including threaded nuts, bushings, pins, and blades. Some types are even available with knurled outer surfaces that help them adhere to plastic.
In addition to being cost-effective, insert molding is environmentally friendly and compatible with many types of materials. Typical inserts are made of metal or plastic. Depending on the application, stiffening inserts may also be made from wood.
Importance of uniform wall thickness
 The uniformity of wall thickness is an essential factor in the plastic injection molding process. It not only provides the best processing results, but also ensures that the molded part is consistently balanced. This uniformity is especially important for plastics, since they are poor heat conductors. Moreover, if the wall thickness of an injection molded part varies, air will trap and the part will exhibit a poorly balanced filling pattern.
Uniform wall thickness also helps reduce shrinkage. Different materials have different shrinkage rates. For instance, thick parts take longer time to cool than thin ones. As the part’s thickness increases, cooling time doubles. This relationship is due to the one-dimensional heat conduction equation, which shows that heat flows from the center of the part toward the cooling channel. However, this relationship does not hold for all types of plastics.
The general rule for maintaining uniform wall thickness in injection molded parts is that walls should be no thicker than 3mm. In some cases, thicker walls can be used, but they will significantly increase production time and detract from the part’s aesthetic appeal and functionality. Furthermore, the thickness of adjacent walls should be no thicker than 40-60% of each other.
The uniformity of wall thickness is critical to the overall quality and efficiency of the injection molding process. An uneven wall thickness can cause twisting, warping, cracking, and even collapse. A uniform wall thickness also reduces residual stress and shrinkage. Injection molded parts are more stable when the wall thickness is uniform.
An injection molded part with thick walls can be problematic, especially when the molded parts are shaped like a cube. A non-uniform wall thickness can result in problems and costly retooling. Fortunately, there are solutions to this problem. The first step is to understand the problem areas and take action.
Using 3D printing to fabricate molds
 The use of 3D printed molds allows manufacturers to manufacture a wide range of injection molded parts. However, 3D-printed molds are not as strong as those made from metallic materials. This means that they do not withstand high temperatures, which can degrade them. As such, they are not suitable for projects that require smooth finishing. In order to reduce this risk, 3D-printed molds can be treated with ceramic coatings.
Using 3D printing to fabricate injection molds can help reduce costs and lead times, allowing manufacturers to bring their products to market faster. This process also has the advantage of being highly efficient, as molds made using 3D printing can be designed to last for many years.
The first step in fabricating an injection mold is to design a design. This design can be complex or simple, depending on the part. The design of the mold can be intricate. A simple example of a mold would be a red cup, with an interior and exterior. The interior portion would have a large cone of material protruding from the other side.
Injection molding is an effective way to produce thousands of parts. However, many engineering companies do not have access to expensive 3D printers. To solve this problem, companies should consider using outside suppliers. In addition to speeding up the manufacturing process, 3D printing can reduce the cost of sample parts.
Plastic injection molding still remains the most popular method for high volume production. However, this process requires a large up-front capital investment and takes a while to adapt. Its advantages include the ability to use multiple molds at once, minimal material wastage, and precision dosing. With an increasing number of materials available, 3D printing can be a smart option for companies looking to manufacture a variety of plastic parts.
editor by CX 2023-04-13
injection molding machine parts and functions
Merchandise Description
High-good quality instructional constructing block toys plastic injection molded custom little plastic portion
Detailed Photos
Common data & coverage for our OEM/ODM plastic injection mould:
| Detailed details for mould metal | ||
| Mould content | Hardness | Mould lifestyle |
| P20 | HRC 28-33 | >300,000 pictures |
| 718 | HRC 33-36 | >500,000 pictures |
| H13 | HRC >43 | >800,000 pictures |
| 2344 | HRC >48 | >800,000 photographs |
| S136 | HRC 48-fifty two | >1,000,000 pictures |
Guide Time :
| Quantity(Sets): | one – 1 | >1 |
| Est. Time(working day): | 30~45 | To be negotiated |
| Description of Ambition Plastic Injection Moulds: | |
| Mould materials: | 45#, P20, 718, 2738, NAK80, S136, H13, 1.2344 etc. |
| Mould base: | LKM, HASCO, and many others. |
| Regular Element: | DME, HASCO, JIS, and so on. |
| Cavity: | One/Multi |
| Runner: | Sizzling/Chilly |
| Mould daily life: | ten,0000~5,000,000shots |
| Design and style software: | UG, PROE, CAD, SolidWorks, and so forth. |
| Plastic substance: | PP, Pc, PE, PS, PU, Abdominal muscles, PVC, PA, POM, PMMA, PET, PPR, and many others. |
| Delivery time: | 40–60days |
| Package deal: | Wooden Case |
| Shipping: | By Sea |
| Specs: | Is dependent on the customer’s specifications |
| Process Machine: | CNC, Substantial-Pace Carver, EDM, Wire Reduce, Driller, Grinder, fly cutter, and many others. |
Ambition Mould Trade Approach:
| 1. Quotation | According to the sample, drawing, and distinct demands. |
| two. Dialogue | Mould materials, cavity quantity, cost, runner, payment, and so on. |
| 3. S/C Signature | Approval for all the products |
| 4. Progress | Spend 50% by T/T |
| five. Item Style Checking | We check the product design and style. If some place is not best, or can not be completed on the mould, we will send out the buyer the report. |
| six. Mould Style | We make mould design and style on the basis of confirmed merchandise patterns and deliver them to the customer for affirmation. |
| seven. Mold Tooling | We start off to make mildew soon after the mould design verified |
| 8. Mildew Processing | Send report to customer as soon as each 7 days |
| nine. Mould Screening | Send out demo samples and try-out stories to the client for affirmation |
| 10. Mildew Modification | According to the customer’s opinions |
| 11. Stability Settlement | 50% by T/T soon after the customer approves the trial sample and mould good quality. |
| twelve. Delivery | Shipping by sea or air. The forwarder can be selected by your aspect. |
Organization data:
Established in 2571, We are focused to offering our buyers with the greatest amount of plastic mold manufacturing & injection molding solutions.
We often insist on the concept of consumer gratification and traits. We have set some illustrations of customers in different international locations for new client referrals. We truly hope that we can develop a lengthy-time period business partnership with CZPT cooperation with you.
We can make all types of plastic injection mould which includes automotive part moulds, beauty component moulds, health-related portion molds, property equipment moulds, electronic element moulds and so on.
We have rich knowledge in making customized plastic injection mould. Send me the inquiry with the drawing and need (steel raw substance, cavity no. and many others) for mould, and I will reply to you in 24 several hours and quotation for you inside of 2 working days.
Why Choose Us:
| Greatest style, aggressive price |
| More than ten years’ Prosperous encounter in this subject |
| Expert in design and style & making plastic mould |
| 1 end remedy |
| On-time supply |
| Best soon after-sale support |
| Specialized in all sorts of plastic injection moulds |
Packaging & Shipping:
FAQ:
one. Q: I have an idea for a new product, but I don’t know if it can be manufactured. Can you help?
A: Yes! We are always happy to work with potential customers to evaluate the technical feasibility of your idea or design and we can advise on materials, tooling, and likely set-up costs.
2. Q: What are the advantages of obtaining my parts manufactured locally?
A: We can offer quick reaction times to any changes in specification, batch size, or material. We can ship small or large quantities anywhere in North The usa, and Europe overnight to accommodate unforeseen changes in demand.
3. Q: My components have already been developed in CAD. Can you use the drawings?
A: Yes! DWG, DXF, IGES, Solid works and STP, X_T files can all be used to generate quotes, models, and mold tools – this can save time and money in producing
your parts.
4. Q: Can I test my idea/component before committing to mold tool manufacture?
A: Yes, we can use CAD drawings to make Prototype models for design and functional evaluations or market exams.
5. Q: What type of plastic is best for my design/ingredient?
A: Materials selection depends on the application of your design and the environment in which it will function. We will be happy to discuss the alternatives and suggest the best material.
six. Q: What type of mould tool do I need?
A: Mould tools can be either a single cavity (one part at a time) or multi-cavity (2,4, 8, or 16 parts at a time). Single-cavity tools are generally used for small quantities, up to 10,000 parts per year whereas multi-cavity tools are for larger quantities. We can look at your projected annual requirements and recommend the
ideal tooling option for you.
seven. Q: Okay, I’ve decided to go ahead with my project. How long will it take to get my parts?
A: It can take 3 to 6 weeks to have the mould tool manufactured depending on the part’s complexity, dimension, and the number of impressions/ cavities (single or multiple). After we receive your final approval on the tool’s preliminary design and style, you can expect delivery of T1 parts within 3-6 months. And throughout the mold developing procedure, mold builds Weekly Update will be supplied to you each and every 7 days for your far better comprehending of the production progress in our workshop.
|
US $1,000-20,000 / Set | |
1 Set (Min. Order) |
###
| Warranty: | 3 Years |
|---|---|
| Shaping Mode: | Injection Mould |
| Surface Finish Process: | Polishing |
| Mould Cavity: | Multi Cavity |
| Plastic Material: | ABS |
| Process Combination Type: | Single-Process Mode |
###
| Samples: |
US$ 0.5/Piece
1 Piece(Min.Order) |
|---|
###
| Customization: |
Available
|
|---|
###
| Detailed info for mould steel | ||
| Mould material | Hardness | Mould life |
| P20 | HRC 28-33 | >300,000 shots |
| 718 | HRC 33-36 | >500,000 shots |
| H13 | HRC >43 | >800,000 shots |
| 2344 | HRC >48 | >800,000 shots |
| S136 | HRC 48-52 | >1,000,000 shots |
###
| Quantity(Sets): | 1 – 1 | >1 |
| Est. Time(day): | 30~45 | To be negotiated |
###
| Description of Ambition Plastic Injection Moulds: | |
| Mould material: | 45#, P20, 718, 2738, NAK80, S136, H13, 1.2344 etc. |
| Mould base: | LKM, HASCO, etc. |
| Standard Component: | DME, HASCO, JIS, etc. |
| Cavity: | Single/Multi |
| Runner: | Hot/Cold |
| Mould life: | 10,0000~5,000,000shots |
| Design software: | UG, PROE, CAD, SolidWorks, etc. |
| Plastic material: | PP, PC, PE, PS, PU, ABS, PVC, PA, POM, PMMA, PET, PPR, etc. |
| Delivery time: | 40–60days |
| Package: | Wooden Case |
| Delivery: | By Sea |
| Specifications: | Depends on the customer’s requirements |
| Process Machine: | CNC, High-Speed Carver, EDM, Wire Cut, Driller, Grinder, fly cutter, etc. |
###
| 1. Quote | According to the sample, drawing, and specific requirements. |
| 2. Discussion | Mold material, cavity number, price, runner, payment, etc. |
| 3. S/C Signature | Approval for all the items |
| 4. Advance | Pay 50% by T/T |
| 5. Product Design Checking | We check the product design. If some position is not perfect, or can not be done on the mould, we will send the customer the report. |
| 6. Mould Design | We make mould design on the basis of confirmed product designs and send them to the customer for confirmation. |
| 7. Mold Tooling | We start to make mold after the mold design confirmed |
| 8. Mold Processing | Send report to customer once each week |
| 9. Mold Testing | Send trial samples and try-out reports to the customer for confirmation |
| 10. Mold Modification | According to the customer’s feedback |
| 11. Balance Settlement | 50% by T/T after the customer approves the trial sample and mould quality. |
| 12. Delivery | Delivery by sea or air. The forwarder can be designated by your side. |
###
| Best design, competitive price |
| Over 10 years’ Rich experience in this field |
| Professional in design & making plastic mould |
| One stop solution |
| On-time delivery |
| Best after-sale service |
| Specialized in all kinds of plastic injection moulds |
|
US $1,000-20,000 / Set | |
1 Set (Min. Order) |
###
| Warranty: | 3 Years |
|---|---|
| Shaping Mode: | Injection Mould |
| Surface Finish Process: | Polishing |
| Mould Cavity: | Multi Cavity |
| Plastic Material: | ABS |
| Process Combination Type: | Single-Process Mode |
###
| Samples: |
US$ 0.5/Piece
1 Piece(Min.Order) |
|---|
###
| Customization: |
Available
|
|---|
###
| Detailed info for mould steel | ||
| Mould material | Hardness | Mould life |
| P20 | HRC 28-33 | >300,000 shots |
| 718 | HRC 33-36 | >500,000 shots |
| H13 | HRC >43 | >800,000 shots |
| 2344 | HRC >48 | >800,000 shots |
| S136 | HRC 48-52 | >1,000,000 shots |
###
| Quantity(Sets): | 1 – 1 | >1 |
| Est. Time(day): | 30~45 | To be negotiated |
###
| Description of Ambition Plastic Injection Moulds: | |
| Mould material: | 45#, P20, 718, 2738, NAK80, S136, H13, 1.2344 etc. |
| Mould base: | LKM, HASCO, etc. |
| Standard Component: | DME, HASCO, JIS, etc. |
| Cavity: | Single/Multi |
| Runner: | Hot/Cold |
| Mould life: | 10,0000~5,000,000shots |
| Design software: | UG, PROE, CAD, SolidWorks, etc. |
| Plastic material: | PP, PC, PE, PS, PU, ABS, PVC, PA, POM, PMMA, PET, PPR, etc. |
| Delivery time: | 40–60days |
| Package: | Wooden Case |
| Delivery: | By Sea |
| Specifications: | Depends on the customer’s requirements |
| Process Machine: | CNC, High-Speed Carver, EDM, Wire Cut, Driller, Grinder, fly cutter, etc. |
###
| 1. Quote | According to the sample, drawing, and specific requirements. |
| 2. Discussion | Mold material, cavity number, price, runner, payment, etc. |
| 3. S/C Signature | Approval for all the items |
| 4. Advance | Pay 50% by T/T |
| 5. Product Design Checking | We check the product design. If some position is not perfect, or can not be done on the mould, we will send the customer the report. |
| 6. Mould Design | We make mould design on the basis of confirmed product designs and send them to the customer for confirmation. |
| 7. Mold Tooling | We start to make mold after the mold design confirmed |
| 8. Mold Processing | Send report to customer once each week |
| 9. Mold Testing | Send trial samples and try-out reports to the customer for confirmation |
| 10. Mold Modification | According to the customer’s feedback |
| 11. Balance Settlement | 50% by T/T after the customer approves the trial sample and mould quality. |
| 12. Delivery | Delivery by sea or air. The forwarder can be designated by your side. |
###
| Best design, competitive price |
| Over 10 years’ Rich experience in this field |
| Professional in design & making plastic mould |
| One stop solution |
| On-time delivery |
| Best after-sale service |
| Specialized in all kinds of plastic injection moulds |
Benefits of Injection Molded Parts in Design
Injection molded parts are manufactured from a variety of plastics. You can order samples of your desired product or download CAD drawings free of charge. For more information, visit our product catalog. There are numerous benefits of using injection molded products in your designs. Here are some of them. Injection molded products are cost-effective and highly customizable.
Design for manufacturability
Design for manufacturability (DFMA) is an important part of the design process for injection-molded parts. This process helps to minimize costs and streamline the production process. It also helps in the prevention of problems during the manufacturing process. The process involves several steps that include part geometry, location of critical surfaces, material selection, and dimensioning. It is also crucial to consider the colors and tolerances, which can help to minimize scrap rates.
Design for manufacturability is a vital early stage in the development process to ensure that the product is cost-effective and repeatable. It begins with a thorough understanding of the purpose for which the part is intended. The design process should take into account every aspect of the part, including the material section, tool design, and the production process.
DFM includes guidelines to ensure that the design meets the manufacturing requirements. These guidelines can include good manufacturing practices, as well as good design principles. Good design focuses on the quantity and quality of parts, as well as the complexity of their surfaces and tolerances. The process also focuses on mechanical and optical properties.
Injection molding design for manufacturability can save resources and time. It also reduces the costs of assembly. An injection molder conducts a detailed analysis of these design elements before starting the tooling process. This is not a standalone principle; it should be used in conjunction with other design optimization techniques.
Ideally, a product should be designed for optimum manufacture. This means that it should not have too many parts, or too few. To minimize this, the designer should choose a model that is easy to mold. Also, a design that does not require too many machine operations and minimizes risks.
Plastics used in injection molding
Injection molding is a very versatile process that uses various types of plastic polymers. These plastics are extremely flexible and can be molded to take on any shape, color, and finish. They can also be customized to contain design elements, text, and safety instructions. Plastics are also lightweight, easily recycled, and can be hermetically sealed to prevent moisture from getting into the product.
Plastics are categorized according to their properties, which can be helpful in selecting the right plastic for a particular application. Different materials have different degrees of hardness, which is important when it comes to molding applications. Some are harder than others, while others are more flexible. Plastics are ranked according to their Shore hardness, which was developed by CZPT.
Polystyrene is one of the most common plastics used in injection molding. However, it has a few disadvantages. While it is a good choice for simple products that do not require high strength and are prone to breakage, it is not ideal for items that need to be resistant to heat and pressure.
While many types of plastics are used in injection molding, choosing the right material is very important. The right material can make a big difference in the performance of your product and the cost of your product. Make sure to talk with your injection molding supplier to determine which plastic is right for your project. You should look for a plastic with a high impact rating and FDA approval.
Another commonly used plastic is PMMA, or polystyrene. This plastic is affordable and has a glass-like finish. It is often used for food and beverage packaging and can be easily recycled. This material is also used in textiles.Characteristics of polypropylene
Polypropylene injection molded parts offer an array of benefits, including a high degree of rigidity, excellent thermal stability, low coefficient of friction, and chemical resistance. These plastics are available in two main types, homopolymers and copolymers. Both types offer superior hardness and tensile strength. However, the material does not have the same fire-resistance as PE plastics.
Polypropylene is a colorless, odorless, crystalline solid. It is highly resistant to a variety of chemicals and is shatter-resistant. Its properties make it a great choice for many industrial applications, including packaging and containers for liquids. The material is also highly durable and can last for a very long time without breaking. In addition, it does not absorb or retain moisture, making it ideal for outdoor and laboratory applications.
Polypropylene is widely used for injection molding, and its low cost, flexibility, and resistance to chemical attack make it a popular choice. This material is also a great electrical insulator and has excellent thermal expansion coefficient. However, it is not biodegradable. Luckily, it can be recycled.
During the molding process, the temperature of the mold is a significant factor. Its morphology is related to the temperature and flow field, and a clear correlation between the two factors is essential. If you can control the temperature and flow, you can optimize your manufacturing process and eliminate costly trial-and-error procedures.
Polypropylene is an excellent electrical insulator and has a high dielectric coefficient. It can also be sterilized and resist high temperatures. Although it is less rigid than polyethylene, it is a good choice for applications where electrical insulation is necessary.
Texture of injection molded parts
Texture design is a common feature of injection molded parts, which helps to raise the perceived value of the vehicle. While traditional manufacturing processes can produce limited textures, additive manufacturing allows for infinite designs. For example, a design that looks like a wood grain pattern may be printed on an aluminum car part.
Texture is important because it can improve the strength of the part and enhance its adhesion to other surfaces. Moreover, textured parts can resist damage from contact and fingerprints. This makes them more durable and a good option for further molding operations. Injection molding processes usually follow a set of standards from the Society of Plastics Industry, which define different types of surface finishes.
Textured plastic injection molded parts may have various types of surfaces, including wood grain, leather, sand, or stipple. Choosing the right surface texture is crucial for enhancing the appearance of the part, but it must also be compatible with its function. Different materials have different chemical and physical properties, which can influence the type of texture. Moreover, the melting temperature of the material is important for its surface finish. The additives used in the process can also have an impact on the surface finish.
Texture can also vary between manufacturers and types of components. Some textures are flat, while others are rough. The top row corresponds to A3 and B4 in flatness, while the bottom row shows rough surfaces. These rough surfaces may damage sensitive testing equipment. However, some textures may have near equivalence with each other, namely SPI D-3 and MT-11020.
The type of texture that is applied to injection molded parts can affect the minimum draft angle required for the parts to be ejected. Parts with light texture tend to be smoother than parts with heavy textures, while parts with heavy textures require a higher draft angle. The draft angle for heavy textures should be between five and 12 degrees. It is best to consider this early in the design process and consult with the injection molder to get a good idea of the necessary draft angles.
editor by czh 2023-03-23
China Plastic Manufacturer Plastic Injection Mould Factory Plastic Injection Moulded Machine Spare Parts Accessories with Hot selling
Design Quantity: DELI
Plastic Modling Kind: Mould
Processing Service: Moulding, Slicing
Substance: Stomach muscles,Personal computer, /Abdominal muscles,PP/TPE/TPR,and so forth
Coloration: Virtually all PMS colours available
Purpose: Industrial parts/daily source/Healthcare grade provide, etc.
Mildew Materials: S136H, 718H, NAK80, P20, H13, and many others.
Surface Therapy: Matte, Widespread sprucing, Mirror polishing, Texture, and many others.
Drawing Format: .stp/.action/.igs/.stl/.dwg/.pdf
Mould Life-cycle: one hundred,000-500,000 photographs
Sample: Offered. A single cavity sample mold or 3D printing
Packing: Pack in bulk/poly bag/bubble bag/colour box
Parameter: Inch, centimeter, millimeter, etc.
Packaging Particulars: Color Box+Abrased CPE Bag
Port: HangZhou Port
| Item | Custom Stomach muscles Plastic areas Injection Molding Support with injection molding |
| Material | ABS, Personal computer/Abdominal muscles, PP, Personal computer, POM(Acetal/Delrin), Nylon 6, Nylon Formed Areas Abs Injection Molded Areas Tailored Plastic Injection CZPT Scenario Nylon 6/6, PA 12, HDPE, LDPE, PS(HIPS), PMMA(Acrylic), SAN/AS, ASA, PVC, UPVC,TPE, TPR, PU, TPU, PET, PEI(Ultem), PSU, PPSU, PPE/PS, PTFE, GPPS, PPS, PPO, PES, CA, and so forth. |
| Certificate | IATF 16949:2016 / ISO 9001:2015 / ISO 45001:2018 / ISO 14001:2015 /Achieve/ROHS/MSDS/LFGB/F D A |
| Drawing Structure | .stp / .action / .igs /.stl /.dwg / .pdf |
| Color | Almost all PMS shades accessible. |
| Parameter | Inch, Custom made Plastic items injection mould processing plastic mold product components centimeter, millimeter, and so on. |
| Function | Industrial elements /every day provide / Health care grade source, and so forth. |
| Surface Remedy | Matte, Typical sharpening, Mirror sharpening, Texture, Plating, Power Coating (Painting), Laser Engraving, Brushing, Marbling,Printing etc. |
| Mold Content | S136H, 718H, NAK80, P20, H13, etc. |
| Mold Precision | If no specific request, apply to SJ/T10628-1995 expectations, class 3. |
| Mold Daily life-cycle | 100,000-500,000 pictures. |
| Packing | Pack in bulk / poly bag / bubble bag / coloration box. |
| Sample | Available. 1 cavity sample mildew or 3D printing. |
| Price Tips | The value proven over is just for reference, closing true cost depends on your layout, substance request, surface remedy, orderqty, China Manufacturer Customized Plastic Button Electronic Device Plastic Parts Injection Molding for Tiny Molded Elements package ask for, and many others. |
Advantages of Injection Moulding
Whether you’re considering an injection molded part for your next project or need to replace an existing one, there are a few factors you should consider. These include design, surface finishes, tooling costs, and material compatibility. Understanding these factors can help you make the right decision. Read on to learn more about the advantages of injection molding and how to get started.
Design factors
 One of the most critical design factors for injection molded parts is the wall thickness. The wall thickness affects many key characteristics of the part, from its surface finish to its structural integrity. Proper consideration of this factor can prevent costly delays due to mold issues or mold modifications. To avoid this problem, product designers must carefully consider the functional requirements of the part to determine the minimum and nominal wall thickness. In addition, they must also consider acceptable stress levels, since parts with excessively thin walls may require excessive plastic pressure and may create air traps.
Another factor to consider when designing a part is its ejection and release capabilities. If the part is released from the mold, the tools should be able to slide the plastic out. Injection molds usually have two sides, one of which is ejectable, and another that remains in the mold. In some cases, special features are required to prevent part release, such as a ramp or a gusset. These design features can increase the design flexibility, but they can also increase the cost of the mold.
When designing injection molded parts, the engineering team first determines the key design elements. These elements will make sure the injection process goes as smoothly as possible. This includes factors like wall thickness, rib design, boss design, corner transition, and weld line, among others. The engineering team will then perform a design for manufacturability analysis and, if all is well, can start building and testing the mold.
Material compatibility
Several factors can affect material compatibility of injection molded parts. When molding plastic parts, it is important to choose a material that is compatible with the part’s intended purpose. Many injection molding processes require that the two main plastic materials used are compatible with each other. This is the case in overmolding and two-shot injection molding.
The material you use to make an injection molded part will significantly impact the tolerance of the finished product. This is why material selection is as important as the design of the part. Many types of plastic resins can be used for injection molding. In addition, many of these resins can be modified or strengthened by adding additives, fillers, and stabilizers. This flexibility allows product teams to tailor the material to achieve desired performance characteristics.
One of the most common thermoplastics is polypropylene. It is extremely durable and has good impact strength and moisture resistance. This material is also recyclable and does not react with food.
Tooling costs
One of the largest costs for manufacturing injection molded parts is tooling. For an OEM, tooling costs can range from $15K per part for a simple part to $500K for a mold with complex geometry. Tooling costs vary based on the type of steel used and the production volume of the part.
To get a reasonable estimate, companies should have a final design, preliminary design, and sample part to hand when requesting quotes. The dimensions and complexity of the cavity in a mold are crucial in determining the tooling cost, as are the part tolerances. Part tolerances are based on the area covered by the part and its functions within the mold.
The type of mold you need can also impact your tooling costs. Injection molding machines can accommodate many different kinds of molds. Some molds are made from a single mold, while others require multiple molds. Some molds can be complicated, making them unmanufacturable, which in turn drives up the cost of tooling.
The costs for tooling for injection molding are not well known, but they do add up quickly. Many product development teams tend to consider the cost of the injection molding process in terms of direct materials, machine time, and labor, but that cost model often fails to take into account additional components.
Surface finishes
 Surface finishes on injection molded parts are often used to mask defects, hide wear and tear, or enhance a product’s appearance. These finishes can also be useful when the product will come in contact with people’s hands. The surface texture you choose will depend on your desired functionality as well as the way you want to use the product. Generally, rougher textures provide better grip while masking minor molding imperfections. However, they can also make a product more difficult to release from the mold. This means that you may have to increase the draft angle of the mold. In order to get the best surface finish, the toolmaker and product designer must collaborate closely early in the design process.
There are several different surface finishes that can be used for injection molded parts. One type is known as the B-grade finish, and is compatible with a wide variety of injection molding plastics. Another type of finish is called a stone polishing process, and is ideal for parts that have no aesthetic value.
Overhangs
The injection moulding industry refers to overhangs on injection molded parts as “undercuts,” and these can lead to design instability. To minimize undercuts, the design must be parallel to the part’s surface. If an undercut is present, a zigzag parting line can be used.
The overhang is typically a few millimeters shorter than the surface of the mold. It is generally made from a lower-cost plastic material than the part’s surface area. The material used for the overhang should have sufficient strength to fulfill its function. An overhang will also help to prevent the piece from deforming or cracking.
Injection molding can create overhangs around the perimeter of a part. Overhangs are not always necessary; they can be added to parts as desired. Adding an overhang, however, will add substantial tooling costs. As a result, it is better to minimize the overall thickness of a design. However, in some cases an overhang can be useful to make the part look more attractive.
For parts with complex geometries, there are a few options for overhangs. Some manufacturers use side-action molds to form more complex shapes.
CNC machining
CNC machining of injection molded parts is a process that helps manufacturers achieve precise surfaces and shapes for their products. This process typically begins with the milling of the tooling, which is typically made of aluminum or steel. This tooling is then placed in a CNC mill. This machine carves the negative of the final plastic part, making it possible to achieve specific surface finishes. The process can be adapted to create a part with a complex structure or special features.
CNC machining allows the manufacturer to produce high-performance parts. This is possible because MIM parts do not experience induced stresses or internal pressure during the manufacturing process. Furthermore, the parts produced by MIM are more durable than CNC parts. Despite their advantages, CNC machining has its limitations, especially when it comes to design freedom and intricacy. This factor is largely dependent on the software used by the manufacturer or designer.
One drawback of CNC machining is its higher cost. Compared to injection molding, CNC machining is more expensive per part. The reason is that the initial mold cost is relatively high and is spread over a large number of parts. Once the injection molding process has been completed, the cost of the parts produced by this process becomes more competitive with those produced by machined parts. However, the cost gap increases with the volume of parts produced. This cost crossover generally occurs in quantities of at least 100 parts and can reach a maximum of 5000 parts.
Production volume
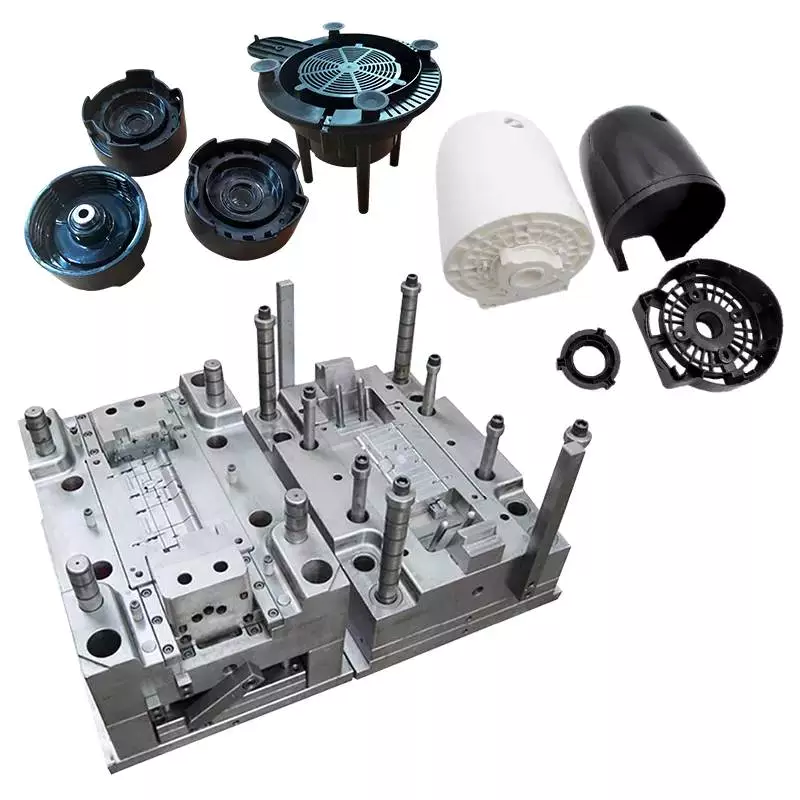 The production volume of injection molded parts varies depending on the material being used. Large volumes of parts are expensive to produce, while small quantities can be produced for low cost. Injection molding requires a precise mold, which is CNC-machined from tool steel or aluminum. The mold has a negative of the part that is injected, a runner system, and internal water cooling channels to aid in cooling the part. Recent advances in 3D printing materials have made it possible to produce molds for low-volume injection molding. Previously, this was not financially viable due to the high cost of traditional mold making.
A mold is used to produce plastic parts. The molding process is very fast, with each cycle taking anywhere from 30 seconds to 90 seconds. After a part is molded, it is removed from the mold and placed on a holding container or conveyor belt. Injection molded parts are generally ready for use right away and require minimal post-processing. Injection molded parts have a similar design to a photograph, since the geometry is directly transferred to the part’s surface texture.
When selecting a plastic mold, it is important to determine the volume that the part will be produced at. If the volume is low, softer plastics may be used. However, as the part is molded over, its performance characteristics may degrade. In low-volume production, it is important to consider the overall complexity of the part. This includes the part’s draft, wall thickness, and surface finish.
editor by czh2023-02-15
China ABS PC PP Injection Products Moulding makingTooling Plastic Auto Parts Custom Plastic enclosure injection molding machine parts and functions
Product Amount: Plastic part08
Shaping Method: Plastic Injection Mould
Item Materials: Plastic
Solution: Exterior, wise merchandise,electroncial solution
Name: Skilled substantial-precision molds and injection molded elements
Shade: white,black,inexperienced,mother nature,blue,yellow,etc
Content: Stomach muscles,PMMA,Computer,PP,PEEK,PU,PA,[email protected] Associate of our European nations around the worldWe have cooperated with them in business for a lot of years, and the prolonged-term cooperation and great top quality have deepened our shut contacts and set up a deep friendship. If we can hope we can be excellent pals R&D layout teamA powerful staff can design very good goods for you, which is why you can decide on us Shipping and delivery and Packaging Sea, land and air transportationShipping by sea, land and air, fast delivery and on time, we can promise the arrival at the specified time FAQ 1. Are you a trading company or a maker?We are a company as you can see our workshop as earlier mentioned.2. What variety of trade conditions can you do?EX-Functions,FOB,CIF,DDP DDU3. What is your conditions of payment?fifty% Mould value deposit,equilibrium mildew expense +fifty% production price compensated when samples confimed,Harmony creation price paid towards duplicate of B/L. We acknowledge T/T4. Do you support OEM ?Yes, we can create by technological drawings or samples.5. How about your shipping and delivery time?Typically, 2571 1-Cease Specialist Ab muscles POM PP Personal computer injection mold areas customised plastic goods provide it take 40 days ( 30 days do mold and 10 days do mass manufacturing).It relies upon on the quantity
What Is Injection Moulding?
Injection molding is a process of producing precision-molded parts by fusing raw plastics and guiding them into a mold. The main components of an injection mold are a hopper, barrel, and reciprocating screw. Before injection, the raw plastics are mixed with coloring pigments and reinforcing additives.
Characteristics of injection molded parts
Injection molding is the process of manufacturing plastic parts. It uses thermoplastic, thermoset, or elastomers to manufacture components. The range of materials is enormous and includes tens of thousands of different polymers. They are blended with other materials and alloys to produce a wide range of properties. Designers select the appropriate materials for the job based on the properties and functions desired in the finished part. During the mold design process, mold materials must be carefully chosen, as different materials require different molding parameters.
Injection molding requires precise tolerances of the temperature and strain levels. The maximum strain level is about 0.15 percent. It is possible to adjust these parameters to meet the requirements of an injection molding project. The resulting products can be easily checked for quality by measuring the strain and temperature of the mold inserts in real time.
Injection molding is known for its laminar flow of the polymer. However, there is still a possibility for side-to-side thermal variations in the part forming cavity. This is illustrated in FIG. 4. The part has high and low sheared areas; the higher sheared areas flow on the bottom side of the part, while the lower sheared areas flow on the top side.
Injection molding is used to make many different types of plastic parts, from small parts to entire body panels of a car. These parts can be made from a variety of different materials, such as polypropylene for toys and ABS for consumer electronics. They can also be made from metal, such as aluminum or steel.
The melting temperature of plastic parts must be appropriate for the project’s specifications. The mold should be large enough to produce the parts desired. This will minimize the impact of uneven shrinkage on the product’s dimensional accuracy. In addition to the temperature, a mold must be designed with the material’s properties in mind.
Tooling fabrication
Injection molded parts are produced using molds. This process is a complex process that requires customization to ensure proper fit and function. The main component of a mold is the base, which holds the cavities, ejectors and cooling lines. The size and position of these components are crucial to the production of quality parts. Incorrectly sized vents can cause trapped air to enter the part during the molding process. This can lead to gas bubbles, burn marks, and poor part quality.
The material used for tooling fabrication is usually H-13 tool steel. This steel is suitable for injection molded parts as it has a low elongation value. The material used to fabricate tooling for injection molded parts typically has a high yield strength. The material used for injection moulding tooling is typically 420 stainless steel or H-13 tool steel. These materials are suitable for most injection molding processes and have comparable yield strength compared to wrought or MIM parts.
Another important part of tooling fabrication is the design of the mold. It is important to design the mold with a draft angle, as this will make ejection easier and reduce costs. A draft angle of 5o is recommended when designing a tall feature. Choosing a draft angle is essential to ensuring that the plastic part is free from air bubbles after injection molding.
Injection moulding tooling costs can account for as much as 15% of the cost of an injection moulded part. With innovation in mould materials and design, tooling fabrication can be more efficient and cost-effective.
Surface finishes on injection molded parts
Surface finishes on injection molded parts can have a variety of effects on the part’s appearance and performance. Different materials lend themselves to different kinds of surface finishes, with some plastics better suited for smooth, glossy finishes than others. The type of surface finish is also affected by several factors, including the speed of injection and the melt temperature. Faster injection speeds help improve the quality of plastic finishes by decreasing the visibility of weld lines and improving the overall appearance of the parts.
For a smooth plastic surface finish, some companies require a high level of roughness on the part. Others may prefer a more rough look, but both options can have their benefits. The type of surface finish chosen will depend on the part’s purpose and intended application. For example, a glossy plastic finish may be preferred for a cosmetic part, while a rougher finish may be better suited for a mechanical part that must be tough and cost-effective.
Surface finishes on injection molded parts are often customized to match the application. For example, some parts require a rough surface finish because they require a greater amount of friction. These parts may require a sandblasting process to achieve the desired texture. Other processes can also be used to control plastic texture.
The type of surface finish depends on the materials used, as well as the design and shape of the part. The type of material used, additives, and temperature also have an impact on the surface finish. It is also important to consider surface finishes early in the design process.
Importance of a secondary operation to improve accuracy
While most injection molded parts do not require secondary operations, some components do require this type of processing. The surface finish of a component will determine how well it functions and what other secondary operations are necessary. Depending on the part’s function, a smooth or textured surface may be appropriate. Additionally, some parts may require surface preparation before applying adhesives, so an accurate surface finish can make all the difference. In order to achieve the desired finish, the injection molder should have experience molding different materials. He or she should also have the knowledge of how to simulate the flow of a mold. Also, experienced molders know how to mix materials to achieve the desired color, avoiding the need for secondary painting processes.
Injection molding is a complex process that requires precision and accuracy. The optimal temperature of the melted plastic must be chosen, as well as the mold itself. The mold must also be designed for the correct flow of plastic. In addition, it must be made of the best thermoplastic material for the part’s design. Finally, the correct time must be allowed for the part to be solid before it is ejected. Many of these issues can be overcome with specialized tooling that is customized to the part’s design.
Injection molding offers the opportunity to make complex parts at low cost. It also allows manufacturers to make parts with complicated geometries and multiple functions.
editor by czh2023-02-13
China 2022 Brother Pe Design Put Customized auto parts plastic injection molding mould parts spare parts tool machine price joining injection molded parts
Error:获取返回内容失败,
Your session has expired. Please reauthenticate.
Designing Injection Molded Parts
Injection molded parts are a great way to produce fast, reliable parts without having to spend much time on post-processing. Whether you’re designing a small component or a large vehicle, you can expect your parts to be ready to use right away. Because of their high-speed production cycles, you can expect your parts to be delivered within 30 to 90 seconds.
Design considerations for injection molded parts
When developing a medical device, there are several design considerations to be made to create a quality injection molded part. Typically, product designers want to minimize the amount of material needed to fill the part while still maintaining the structural integrity of the product. To this end, injection molded parts often have ribs to stiffen the relatively thin walls. However, improper placement of ribs or projections can create molding problems.
Design considerations for injection molded parts include the overall shape and finish of the part. There are several ways to make the part look better. One way is to make the surface smoother and less pronounced. This will help the material flow evenly throughout the mold and minimize the risk of parting lines. Another way to reduce the risk of sink marks is to reduce the thickness of ribs relative to the nominal wall thickness of the part.
A common problem encountered when designing injection molded parts is sink marks. These can be difficult to avoid. A molder may not be willing to guarantee the product’s surface is sink-free, so designers must make sure that sink marks are minimized. To prevent these problems, the design of the parts should be as simple as possible.
Injection molded parts can also have complex geometries, and the design process is incredibly flexible. A good molder will be able to reproduce complex parts at low cost. To get the best possible results, designers should discuss the design and process with the molder. They should also discuss with the molder any critical tolerance specifications. The designer should also consider reworking the mold if necessary.
The wall thickness of a plastic injection molded part should be consistent. This is important because it influences the part’s functionality and performance. An uneven wall thickness can result in sink marks, voids, and other undesirable effects. It may also result in excessive plastic pressure or cause air traps.
Materials used in injection molded parts
When designing a product, materials used in injection molding are an important factor in the end result. These materials vary in strength, reusability, and cost. Understanding these differences is essential for ensuring the best product. In addition, understanding the characteristics of these materials can help you plan your budget and determine which ones are right for your application.
Choosing the wrong material can have serious consequences. In addition to premature component failure, the wrong choice can also increase your cost. To avoid such an occurrence, it’s a good idea to seek expert advice. Expert consultations can help you understand the factors that are important for your particular plastic molding project.
Fortron PPS: This thermoplastic resin offers excellent strength, toughness, and chemical resistance. It’s also stiff and durable, which makes it ideal for demanding industrial applications. Other common plastics include Nylon 6/6, which is strong and lightweight. Its high melting point makes it a great replacement for metal in certain environments. It also offers desirable chemical and electrical properties. PEEK is another common material used in injection molding.
ABS: Another engineering grade thermoplastic, ABS offers excellent heat resistance and chemical resistance. The disadvantage of ABS is its oil-based composition. As a result, ABS production creates noxious fumes. Nylon is another popular plastic for injection molding. Nylon is used in many different applications, from electrical applications to various kinds of apparel.
Injection moulding is a process where raw material is injected through a mold under high pressure. The mold then shapes the polymer into a desired shape. These moulds can have one or multiple cavities. This enables manufacturers to create different geometries of parts using a single mould. Most injection moulds are made from tool steel, but stainless steel and aluminium are also used for certain applications.
Characteristics of injection molded parts
 Injection molded parts exhibit a range of mechanical and physical properties. These properties affect the performance of the parts. For example, they can affect electrical conductivity. Also, the degree of filling in the parts can determine their mechanical properties. Some studies have even found that filling content can affect the dimensional accuracy of the parts.
To ensure the highest quality of the molded parts, it is important to inspect the machines and processes used to manufacture them. Proper maintenance can prevent mistakes and prolong the service life of the components. Moreover, it is essential to clean and lubricate the machine and its components. This will also reduce the possibility of mold errors.
The temperature and pressure characteristics of the injection mold can be characterized with the help of a simulation tool. For example, in a simulation environment, the injection pressure can be set as a profile and is equal to the pressure in the flow front. Moreover, the maximum injection pressure can be set as a value with minimum dependence on the flow rate. The temperature of the material used in the injection mold should be within a recommended range.
The temperature and pressure of the mold cavity must be monitored to ensure proper ejection. The temperature of the injection mold cavity is usually set at a temperature slightly above the ejection temperature. This can be manually or automatically. If the temperature is too high, the part will not be able to eject. The rapid temperature change can cause the part to warp. The same applies to the cooling time of the mold and cavity.
The thickness of the molded part should be uniform. If the injection mold does not conform to the required thickness, sink marks may be visible. A minimum of 2.5 mm between the outer and inner diameters is required for proper ejection.
Common problems encountered
There are several common problems encountered during the production of injection-molded parts. One of the most common of these is sink marks. These appear on the surface of the part and are a result of uneven cooling of the plastic within the mold. This problem can be caused by poor mold design, insufficient cooling time, and/or low injection pressure.
The first common problem occurs when the mold is not tightly clamped. This causes the molten plastic to be forced out of the mold. Other problems may occur due to the wrong clamping pressure or temperature. In these cases, the clamping force should be increased or the mold design should be revised to allow the plastic to flow properly through it. In addition, a poor quality mold may cause flash or burrs.
Another common problem is wavy patterning. These two defects can affect the appearance and functionality of the part. To avoid these problems, work with an experienced injection molding manufacturer who has experience in these types of parts. They will be able to troubleshoot and minimize any potential risks.
One of the most common problems encountered in injection molding is discoloration. A discolored part will be black or rust-colored. This problem is caused by an excess of air in the mold cavity, and can be avoided by reducing the injection speed. Ventilation systems can also be adjusted to minimize the chances of these problems.
Defective molds can cause a negative impact on the bottom line. By understanding the common problems encountered during injection molding, you can better avoid these problems and make your products as attractive as possible.
Fasteners used in injection molded parts
 Injection molded parts often use fasteners for securing fastener elements in place. As shown in FIGS. 7 and 8 (two separate views), the fastener elements are integrated with the molded product, and they extend from one side. The fastener elements are designed to engage loop elements in the overlying layer. The palm-tree shaped fasteners are especially well-suited for this purpose, as their three-dimensional sides engage more loops than flat sides. These features result in a more secure closure.
When fasteners are used in injection molded parts, the plastic is injected into a mold, with the fastener integrated. In addition to self-tapping screws, other plastic fasteners can include moulded or pre-drilled pilot holes. This method avoids the need for a secondary assembly step and ensures an easy fit. These screws also have other advantages, including a smaller thread profile and lower radial stress, which prevents boss damage.
Another type of fastener commonly used in injection molded parts is a boss. This type of fastener is typically larger than the nut and the pilot hole. An undersized boss can lead to warpage during the injection molding process and cause a product to fail in the field.
Another type of fastener used in injection molded parts is a thread insert, which is usually a stainless steel A2 wire. There are different versions of this fastener for different materials, including carbon fiber reinforced plastic. And the fastener can be modified to adjust the size of the hole.
These fasteners are used in many different types of injection molded parts. Some parts are used to fix a variety of cosmetic issues, such as minor sinks. While these are not defects, they may not look perfect, and they can affect the overall appearance of a product. If you want to improve the appearance of an injection molded part, you can add fibers and glass fibers, as well as colorants.
editor by czh2023-02-10
China Custom High Quality Injection Molded Parts Plastic Parts Service injection molding machine parts and functions
Merchandise Description
Personalized Substantial High quality Injection Molded Areas Plastic Components Services
Advantages:
1. Free style and free sample.
2. Signal NDA.
3. ISO Certificated with the stringent high quality handle program.
4. thirteen A long time OEM&ODM Mould-creating,steel and plastic processing experience.
five. Very good at spoken english and phone contact communication.
6.A single quit remedy and fall shipment for on-line sellers.
Item Description
| Item Description | ODM plastic injection molding |
| Plastic Components: | PS, Abs, PP, PVC, PMMA, PBT, Computer, POM, PA66, PA6, PBT+GF, Pc/Abdominal muscles, PEEK, HDPE, TPU, PET, PPO,…and many others. |
| Standard: | ISO9001:2008 |
| Quality: | RoSH and SGS common |
| Characteristic: | Non marking and Non flash |
| Dimensions: | According to your 2d, 3D Drawing |
| Colour,Quantity,Unit value,Tooling expense,Tooling size: | To be discussed |
| Package deal: | Regular exported Picket box packed, Fumigation approach(on essential) |
| Mold Building Direct Time: | T1, fifteen-25 Operating times, Portion measurement report (upon needed). |
| Export Region: | All countries are reachable. |
| Encounter: | thirteen several years experience in plastic injection mould creating and plastic prouducts produce. |
| Mould Base: | Hasco Standard, European Normal, Planet Common |
| Mould Foundation Substance: | LKM, FUTA, HASCO, DME,…and many others. Or as per Customer’s Requirment. |
| Floor End: | Texture(MT standard), High gloss sharpening |
| Cavity/Core Steel: | P20, 2311, H13, 2344, Starvax 420, 236, AdC3, S136, 2312, 2379, 2316, 2083, Nak80, 2767 …and many others. |
| Sizzling/ Cold Runner | HUSKY, INCOE, YDDO, HASCO, DME, MoldMaster, Masterflow, Mastip, ZheJiang manufactured brand…and many others. |
| Mould Life: | 5,000 to 1,000,000 Photographs. (According to your operating environment.) |
| Layout & Program Softwares: | CAD, CAM, CAE, Professional-E, UG, Soild works, Moldflow, CATIA….etc. |
| Equipments: | Large velocity CNC, Standard CNC, EDM, Wire Chopping, WEDM, Grinder, Plastic Injection Molding Device for trial out mildew from 50-3000T obtainable. |
Products present
Providers
Papler Industry offers support of prototype making, mold design and style, mould production, mass creation and assembly services in home. Our expertise range from simple layout to demanding technological elements.
Firm Profile
Workshops and Equipments
Cooperating Clients
Packaging & Delivery
FAQ
1. Q: The place is your business or factory?
A: We are positioned in HangZhou, We have our personal factory.
two. Q: Can you make layout?
A: We’ll be glad to make CZPT types for you, and for free. Comprehensive CZPT 2nd & 3D will source to clients following get.
three. Q: What type of CZPT you can make?
A: We can make all kinds of plastic injection mould, specifically abundant Encounter
on household moulds.
four. Q: What type of files can you acknowledge?
A: We can acknowledge various sorts of data files these kinds of as DXF, DWG, IGS, IGES, STP, PRT, X_T, PDF.
five. Q: What kind of steel do you use?
A: P20, P20 (H), 718, 718 (H), 2738, 2738 (H), H13, NAK80,2344, S136, 4Cr13, S55C,C45#
6. Q: What kind of material you use for examination CZPT and creation?
A:PP, Laptop, PS, PE, HDPE, POM, PA6, PA66, PA6+GF, Abs, TPU, TPE, PVC, SMC, BMC,
We have wealthy experience for producing merchandise with these components and know
how to adjust Parameter to get the excellent item.
7. Q: How to send sample?
A: The quotation we provide you such as The cost of sample supply 2 occasions samples by
DHL, UPS, EMS,FEDEX or TNT.
|
US $0.01-3 / Piece | |
1 Piece (Min. Order) |
###
| Plastic Type: | Thermosetting Plastic |
|---|---|
| Plastic Form: | Powder |
| Molding Method: | Injection Molding |
| Customization: | Available |
| Material: | ABS, PP, Nylon, PC, POM, PU, TPU, TPV, PBT, PC+Ab |
| Drawing: | Provide by Customer(Dxf/Dwg/Prt/Sat/Iges/Step etc) |
###
| Samples: |
US$ 1/Piece
1 Piece(Min.Order) |
|---|
###
| Customization: |
Available
|
|---|
###
| Product Description | ODM plastic injection molding |
| Plastic Materials: | PS, ABS, PP, PVC, PMMA, PBT, PC, POM, PA66, PA6, PBT+GF, PC/ABS, PEEK, HDPE, TPU, PET, PPO,…etc. |
| Standard: | ISO9001:2008 |
| Quality: | RoSH and SGS standard |
| Feature: | Non marking and Non flash |
| Size: | According to your 2D, 3D Drawing |
| Color,Quantity,Unit price,Tooling cost,Tooling size: | To be discussed |
| Package: | Standard exported Wooden box packed, Fumigation process(upon required) |
| Mold Building Lead Time: | T1, 15-25 Working days, Part measurement report (upon required). |
| Export Country: | All countries are reachable. |
| Experience: | 13 years experience in plastic injection mold making and plastic prouducts produce. |
| Mould Base: | Hasco Standard, European Standard, World Standard |
| Mould Base Material: | LKM, FUTA, HASCO, DME,…etc. Or as per Customer’s Requirment. |
| Surface Finish: | Texture(MT standard), High gloss polishing |
| Cavity/Core Steel: | P20, 2311, H13, 2344, Starvax 420, 236, AdC3, S136, 2312, 2379, 2316, 2083, Nak80, 2767 …etc. |
| Hot/ Cold Runner | HUSKY, INCOE, YDDO, HASCO, DME, MoldMaster, Masterflow, Mastip, Taiwan made brand…etc. |
| Mould Life: | 5,000 to 1,000,000 Shots. (According to your working environment.) |
| Design & Program Softwares: | CAD, CAM, CAE, Pro-E, UG, Soild works, Moldflow, CATIA….etc. |
| Equipments: | High speed CNC, Standard CNC, EDM, Wire Cutting, WEDM, Grinder, Plastic Injection Molding Machine for trial out mold from 50-3000T available. |
|
US $0.01-3 / Piece | |
1 Piece (Min. Order) |
###
| Plastic Type: | Thermosetting Plastic |
|---|---|
| Plastic Form: | Powder |
| Molding Method: | Injection Molding |
| Customization: | Available |
| Material: | ABS, PP, Nylon, PC, POM, PU, TPU, TPV, PBT, PC+Ab |
| Drawing: | Provide by Customer(Dxf/Dwg/Prt/Sat/Iges/Step etc) |
###
| Samples: |
US$ 1/Piece
1 Piece(Min.Order) |
|---|
###
| Customization: |
Available
|
|---|
###
| Product Description | ODM plastic injection molding |
| Plastic Materials: | PS, ABS, PP, PVC, PMMA, PBT, PC, POM, PA66, PA6, PBT+GF, PC/ABS, PEEK, HDPE, TPU, PET, PPO,…etc. |
| Standard: | ISO9001:2008 |
| Quality: | RoSH and SGS standard |
| Feature: | Non marking and Non flash |
| Size: | According to your 2D, 3D Drawing |
| Color,Quantity,Unit price,Tooling cost,Tooling size: | To be discussed |
| Package: | Standard exported Wooden box packed, Fumigation process(upon required) |
| Mold Building Lead Time: | T1, 15-25 Working days, Part measurement report (upon required). |
| Export Country: | All countries are reachable. |
| Experience: | 13 years experience in plastic injection mold making and plastic prouducts produce. |
| Mould Base: | Hasco Standard, European Standard, World Standard |
| Mould Base Material: | LKM, FUTA, HASCO, DME,…etc. Or as per Customer’s Requirment. |
| Surface Finish: | Texture(MT standard), High gloss polishing |
| Cavity/Core Steel: | P20, 2311, H13, 2344, Starvax 420, 236, AdC3, S136, 2312, 2379, 2316, 2083, Nak80, 2767 …etc. |
| Hot/ Cold Runner | HUSKY, INCOE, YDDO, HASCO, DME, MoldMaster, Masterflow, Mastip, Taiwan made brand…etc. |
| Mould Life: | 5,000 to 1,000,000 Shots. (According to your working environment.) |
| Design & Program Softwares: | CAD, CAM, CAE, Pro-E, UG, Soild works, Moldflow, CATIA….etc. |
| Equipments: | High speed CNC, Standard CNC, EDM, Wire Cutting, WEDM, Grinder, Plastic Injection Molding Machine for trial out mold from 50-3000T available. |
Designing Injection Molded Parts
Injection molded parts are designed to work together to form a whole. While the small plastic toys like Legos aren’t typically fabricated for assembly, these products still require precision measurements. For this reason, the designs of injection molded parts should be perfected for manufacturing. The designs should also minimize error potential.
Design considerations for injection molded parts
 When designing injection molded parts, it’s essential to consider the wall thickness of the part. Ideally, the wall thickness is uniform across the entire part. This allows the entire mold cavity to fill without restriction, and reduces the risk of defects. Parts that don’t have uniform wall thickness will have high stresses at the boundary between two sections, increasing the risk of cracks, warping, and twisting. To avoid such stresses, designers can consider tapering or rounding the edges of the part to eliminate stress concentration.
The wall thickness of the injection molded part is important because it affects many key characteristics. Therefore, it is critical to take proper care in choosing the wall thickness to avoid costly delays caused by mold problems or mold modification. The nominal wall thickness should be determined based on the function and stress requirements of the part. Similarly, the minimum wall thickness should be calculated based on acceptable stress. Too thin a wall can result in air traps and excessive plastic pressure.
Injection molded parts that have sharp corners are a common cause of defects. Sharp corners create stress concentrations, poor flow patterns, and increased injection mold wear. To minimize these problems, designers should keep inside corners and outside corners at half the wall thickness. This will help minimize stress and ensure the integrity of the part.
Another important design consideration for injection molded parts is the thickness of the ribs. They should be at least two-thirds of the outer wall. Thicker ribs may result in sink marks on the outer surface. Undercuts also complicate the mold design and increase the cost of the part.
Tolerance variation is also an important consideration. It depends on materials, process control, and tool design. Tolerance variation varies from molder to molder, and designers should discuss critical tolerance requirements with molders. If the part has to be manufactured to a particular tolerance, designers should consider options for mold revisions to minimize the tolerance variance. Additionally, designers may need to intentionally design extra clearance. To compensate for such variation, the molder may remove some steel or modify the design. In some cases, interference can be solved by welding.
Design considerations for injection molded parts should be discussed with material science professionals early in the design process. This is critical because changes to the mold design can be costly. Therefore, achieving the best possible result is critical. By following design guidelines, manufacturers can avoid common defects. A uniform wall thickness is also important because non-uniform thickness can lead to warping the part as it cools.
Another important factor for injection molded parts is the flowability of the material in the mold cavity. The resin should be able to flow easily around rounded corners. For example, a molded part with a curved undercut will not eject properly from the mold if there’s no space between the two sides. For this reason, designers should consider the flowability of the molded material before deciding on a design.
Adding a runner system to an injection molding machine
 There are two main types of runner systems: hot runner systems and cold runner systems. In a hot runner system, a runner nozzle delivers the molten plastic into the mold cavity. A cold runner system does not require the use of a nozzle and acts as a conduit for the molten plastic.
The design of a hot runner mold should balance the activity of plastic solution and mold cavities. Ideally, a mold with two cavities is better balanced than one with three. However, it is important to remember that a three-cavity mold requires a manifold balance of human activities.
Plastic mold runner systems are crucial for ensuring consistent fill rates and pressure. Whether you are producing single or multiple-cavity plastic parts, a runner system will keep your processes consistent. When choosing a runner system, make sure you have the right one for your application.
Hot runner systems can reduce cycle times by as much as 10 to 30 percent. They help improve quality control and minimize material waste by keeping the plastic molten throughout the molding process. Moreover, they help save on plastic raw materials and energy. These features make them ideal for large production lines.
A hot runner system can also help prevent overfilling a cavity. Make sure that the volume of the hot runner is equal to the volume of the mold cavity. Otherwise, the plastic solution will be trapped inside the hot runner for too long and decompose.
Hot runner systems come in many varieties. One type of hot runner system is called the sprue hot runner system. This system uses a mechanical valve to open and close a nozzle. This type of hot runner is more effective and efficient than a general-purpose hot runner. However, it is also more expensive.
In a three-plate mold, the runner system is positioned between the core and cavity plates. When the mold is opened, the runner system automatically separates from the molded part. This eliminates the need for manual labor, but increases the cost of tooling.
The runner system is important for producing parts that are both thin and thick. The runner should be narrow but large so as not to create voids and improve the overall performance of the final product. Runner systems are also important for reducing the amount of energy needed to form and regrind the material.
A hot runner system is one way to improve the speed and accuracy of plastic molding. It helps avoid problems with waste by reducing the amount of plastic wasted. Furthermore, a hot runner system also prevents expensive repairs. By adding a runner system to an injection molding system, you will ensure better quality and precision, and avoid unnecessary downtime and costly repairs.
Hot runner systems are ideal for high-volume productions. However, they require a higher level of maintenance. In addition, hot runner systems are difficult to clean and often leave waste material. Hidden runners may also be inconvenient to remove, especially when changing materials or colors. They can also lead to sticking issues if they are made from thermally sensitive materials.
Using a thermally isolated cold injection unit
 Thermostatic control of temperature in an injection molding process can make a significant impact on part quality. High mold temperatures should be regulated by using a temperature-controlled cooling unit. These devices are equipped with pumping systems and internal heaters. The temperature of the injected plastic determines the plastic’s flow characteristics and shrinkage. Temperature also influences the surface finish, dimensional stability, and physical properties of the finished product.
A thermally isolated cold injection unit allows mold operators to mold parts at lower temperatures than a conventional injection molding machine. The injection mold itself is composed of two steel halves. The two halves are connected by a mechanical hinge. During injection molding, a small amount of plastic is forced into the mold cavity. The injected plastic is then allowed to cool into a solid state. The molded part then falls out of the mold halves. The injected part then enters a bin to be collected.
The heat/cool injection molding process can improve the aesthetics of molded parts significantly. The effects of this technique are particularly apparent with amorphous resins, which do not form a skin during the injection phase. The molded parts have a higher gloss than with conventional molding techniques.
This process requires less clamping force than conventional injection molding and offers more design freedom. It also increases process capacity and materials savings. The process control for this process is more complex, with variables such as the amount of melt injection, water pressure, and water injection delay time.
The angle of repose is another criterion. A low angle indicates that the pellets are free-flowing, while an angle above 45deg indicates that the pellets are not free-flowing. This is important when processing nylon resins.
Plastic injection molding has made huge advances in recent decades. Today, most injection molds fall into one of two types: hot runner and cold runner. Each has its advantages and disadvantages. Understanding how they differ will help you decide which method is right for you.
Injection molding is a highly effective manufacturing process that gives manufacturers a competitive edge over their competition. Using this process produces high-quality plastic and metal parts with minimal waste and a low cycle time. The process is also extremely accurate and produces products with the perfect blend of flexibility and strength.
editor by czh 2022-12-31
China ABS Plastic Injection Molding Parts injection molding machine parts and functions
Item Description
|
Specifications FOR FANG CZPT INJECTION MOULDS |
|||
|
Injection mould normal |
HASCO, DME, MISUMI, China lKM Standard |
||
|
Please give |
2nd, 3D, samples, or the size of the multi-angle photos |
||
|
Mould content |
45#, 50#, P20, 738, 738H, 718, 718H, NAK80, 2316, 2316A, S136, S136H etc |
||
|
Solution material |
Stomach muscles, PA6, PA66, PP, Computer, TPU, POM, PBT, PVC, TPE, TPV, TPO, TPR, PE, HDPE etc |
||
|
Cavity |
Single-cavity, Multi-cavity or by asked for |
||
|
Runner technique |
Chilly runner or Sizzling runner |
||
|
Mould precision |
±0.01mm |
||
|
Mould Lifestyle |
fifty-100 million photographs |
||
|
Software |
CAD, Pro-E, UG, Rhinoceros and so forth |
||
|
Design and style Time |
one-3 days (typical conditions) |
||
|
Principal thechnology |
Milling, grinding, CNC, EDM, wire reducing, carving, EDM, lathes and so forth |
||
Organization Profile
Our company offers a broad variety of items to meet up with your requirements. Given that the institution of our firm, we insist on the management plan of “top quality initial, customer very first and credit oriented”, and often try out our very best to meet up with the potential needs of our buyers. The craze of financial globalization is developing with an unstoppable drive, and our firm is ready to cooperate sincerely with enterprises all in excess of the entire world to obtain a CZPT scenario.
HangZhou CZPT Plastic Products Co., Ltd. is a producer specializing in mold creating and injection molding, which was proven in China in 2013.
Above the several years, we have been dedicated to supplying our customers with high good quality numerous molds and molded components and less time.
We have our own R&D section to supply technological assist. Presently, our business scope contains injection molds, blow molds, die casting molds, 3D printing, and our primary items incorporate automotive elements, aerospace parts, electronic elements, healthcare merchandise, residence equipment areas, and many others
. We have the ability to take your
merchandise from conception to completion. Welcome to HangZhou CZPT Plastic Goods Co.
Workshop
Custom Procedure
Tailored injection mold measures
1. Buyers will give 3D drawings or sample inquiry, and we will quotation according to 3D drawings or samples.
two. Negotiations incorporate mildew value, mould high quality, mildew material, mould cavity content, mildew dimensions, area effects, complex demands, mildew existence, warranty period, item weight, merchandise expense, shipping time, logistics method, payment method, and so on.
3. Confirm the buy. Proforma bill or professional bill.
four. T/T deposit. 50% T/T in advance ,equilibrium ahead of cargo.
five. DFM (Design For Production), Make sure high quality. CZPT style, CZPT drawing confirmation.
six. Mold processing. Comments the processing progress each week, we will demonstrate you the photographs of mould processing.
7. Sample confirmation. Specific sample, affirm sample, mass generation.
8. Item packaging. Picket case, carton or customized created.
9. Shipping. By Sea, By air, etc. Pay the balance.
Certifications
Our Benefits
Why Clients Pick Us?
| We have been engaged in this discipline for fifteen a long time, we’ve served consumers from the United States, the United Kingdom, Spain, Australia, Singapore, Russia and other nations around the world. |
| Professional Certification |
| Quality handle and technological innovation enhancement |
| •ISOIS09001:2000 |
| •SGS certification |
| •The total quality management technique. |
| Precision sturdy mould |
| •3 CNC: Precision .005mm |
| •1 Three dimension:1Precision .001mm |
| •1 wire push gradually: Precision .002mm |
| •2 Mirror discharge: Precision .005mm |
| one hundred% Assured Good quality |
| •100% analyzed(Not Just Batch Tested) |
| •SOP normal manufacturing |
| •IQC(examined all in matical )-IPQC(examined initial elements and prodcut)-FQC(tested finished parts)-OQC(Shipments) |
| •10 specialist high quality management inspectors |
| Aggressive value and support |
| •Delivery time: 2-3 Months after purchase |
| •Provide new design and style for customers’ demands |
| •Provide DFM Report,Moldflow,Mould Design and style,MPR,QC Report, Injection parameter sheet,Tests video. |
| •Free provided sample. |
| •10-20% less costly than other rivals |
| •Return the total CZPT cost if you order five hundred,000pcs item. |
| •Life-long promise time period, which is a lot more time amongst this discipline. |
FAQ
China Company Precision Injection Mold Plastic Injection Mold / Metal CZPT Producing Plastic Mold
1. Are you buying and selling firm or factory?
We are factory with 10 many years knowledge.
two. How lengthy will consider for the sample?
Generally the sample time will 3-5 working times. Specific time in accordance to the item composition
3. Is it achievable to know the production circumstance with out checking out your manufacturing unit?
Detailed manufacturing plan will offer you to you when the item comfirmed. In addition, movie will be sent to you throughout the manufacturing method.
4. What do i need to have to offer for your quoted?
Make sure you send to us your drawing and thorough prerequisite. such as content, quantity, surface therapy and so on. quotation will be send out to you in 8 several hours
5. What’s your conditions of payment?
30% deposit in advance, 70% balance ahead of shipping. T/T, L/C, Escrow, Paypal and Western Union are available.
Personalize your own moulds in MOLDOR PLASTIC !
* In-home mildew design and constructing capabilities to Enhance function efficiency.
* Manufacturing unit value helps make your cost clear.
* NDA agreement can be signed to protect customers’ idea and layout.
* Expert product sales group. Excellent conversation abilities and after-services.
* Professional design and style crew, mildew maker engineer. OEM/ODM services.
* Expert QC and R&D groups to guarantee higher good quality.
* In time reaction to letters and emails.
* On time delivery.
|
US $0.3-0.5 / Piece | |
1,000 Pieces (Min. Order) |
###
| Material: | PVC PC ABS POM TPU TPR PP |
|---|---|
| Application: | Medical, Household, Electronics, Automotive, Agricultural |
| Certification: | RoHS, ISO |
| Die Material: | 45#, 50#, P20, 738, 738h, 718, 718h, Nak80, 2316, |
| Main Thechnology: | Milling, Grinding, CNC, EDM, Wire Cutting, Carving |
| Mould Life: | 50-100 Million Shots |
###
| Customization: |
Available
|
|---|
###
|
SPECIFICATIONS FOR FANG RUI INJECTION MOULDS
|
|||
|
Injection mold standard
|
HASCO, DME, MISUMI, China lKM Standard
|
||
|
Please provide
|
2D, 3D, samples, or the size of the multi-angle pictures
|
||
|
Mould material
|
45#, 50#, P20, 738, 738H, 718, 718H, NAK80, 2316, 2316A, S136, S136H etc
|
||
|
Product material
|
ABS, PA6, PA66, PP, PC, TPU, POM, PBT, PVC, TPE, TPV, TPO, TPR, PE, HDPE etc
|
||
|
Cavity
|
Single-cavity, Multi-cavity or by requested
|
||
|
Runner system
|
Cold runner or Hot runner
|
||
|
Mould precision
|
±0.01mm
|
||
|
Mould Life
|
50-100 million shots
|
||
|
Software
|
CAD, PRO-E, UG, Rhinoceros etc
|
||
|
Design Time
|
1-3 days (normal circumstances)
|
||
|
Main thechnology
|
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes etc
|
||
###
| We have been engaged in this field for 15 years, we’ve served customers from the United States, the United Kingdom, Spain, Australia, Singapore, Russia and other countries. |
| Professional Certification |
| Quality control and technology improvement |
| •ISOIS09001:2000 |
| •SGS certificate |
| •The complete quality control system. |
| Precision durable mold |
| •3 CNC: Precision 0.005mm |
| •1 Three dimension:1Precision 0.001mm |
| •1 wire drive slowly: Precision 0.002mm |
| •2 Mirror discharge: Precision 0.005mm |
| 100% Guaranteed Quality |
| •100% tested(Not Just Batch Tested) |
| •SOP standard production |
| •IQC(tested all in matical )-IPQC(tested first parts and prodcut)-FQC(tested finished parts)-OQC(Shipments) |
| •10 professional quality control inspectors |
| Competitive price and service |
| •Delivery time: 2-3 Weeks after order |
| •Provide new design for customers’ requirements |
| •Provide DFM Report,Moldflow,Mould Design,MPR,QC Report, Injection parameter sheet,Testing video. |
| •Free provided sample. |
| •10-20% cheaper than other competitors |
| •Return the entire mould cost if you order 500,000pcs product. |
| •Life-long guarantee period, which is much longer among this field. |
|
US $0.3-0.5 / Piece | |
1,000 Pieces (Min. Order) |
###
| Material: | PVC PC ABS POM TPU TPR PP |
|---|---|
| Application: | Medical, Household, Electronics, Automotive, Agricultural |
| Certification: | RoHS, ISO |
| Die Material: | 45#, 50#, P20, 738, 738h, 718, 718h, Nak80, 2316, |
| Main Thechnology: | Milling, Grinding, CNC, EDM, Wire Cutting, Carving |
| Mould Life: | 50-100 Million Shots |
###
| Customization: |
Available
|
|---|
###
|
SPECIFICATIONS FOR FANG RUI INJECTION MOULDS
|
|||
|
Injection mold standard
|
HASCO, DME, MISUMI, China lKM Standard
|
||
|
Please provide
|
2D, 3D, samples, or the size of the multi-angle pictures
|
||
|
Mould material
|
45#, 50#, P20, 738, 738H, 718, 718H, NAK80, 2316, 2316A, S136, S136H etc
|
||
|
Product material
|
ABS, PA6, PA66, PP, PC, TPU, POM, PBT, PVC, TPE, TPV, TPO, TPR, PE, HDPE etc
|
||
|
Cavity
|
Single-cavity, Multi-cavity or by requested
|
||
|
Runner system
|
Cold runner or Hot runner
|
||
|
Mould precision
|
±0.01mm
|
||
|
Mould Life
|
50-100 million shots
|
||
|
Software
|
CAD, PRO-E, UG, Rhinoceros etc
|
||
|
Design Time
|
1-3 days (normal circumstances)
|
||
|
Main thechnology
|
Milling, grinding, CNC, EDM, wire cutting, carving, EDM, lathes etc
|
||
###
| We have been engaged in this field for 15 years, we’ve served customers from the United States, the United Kingdom, Spain, Australia, Singapore, Russia and other countries. |
| Professional Certification |
| Quality control and technology improvement |
| •ISOIS09001:2000 |
| •SGS certificate |
| •The complete quality control system. |
| Precision durable mold |
| •3 CNC: Precision 0.005mm |
| •1 Three dimension:1Precision 0.001mm |
| •1 wire drive slowly: Precision 0.002mm |
| •2 Mirror discharge: Precision 0.005mm |
| 100% Guaranteed Quality |
| •100% tested(Not Just Batch Tested) |
| •SOP standard production |
| •IQC(tested all in matical )-IPQC(tested first parts and prodcut)-FQC(tested finished parts)-OQC(Shipments) |
| •10 professional quality control inspectors |
| Competitive price and service |
| •Delivery time: 2-3 Weeks after order |
| •Provide new design for customers’ requirements |
| •Provide DFM Report,Moldflow,Mould Design,MPR,QC Report, Injection parameter sheet,Testing video. |
| •Free provided sample. |
| •10-20% cheaper than other competitors |
| •Return the entire mould cost if you order 500,000pcs product. |
| •Life-long guarantee period, which is much longer among this field. |
Advantages of Injection Moulding
Whether you’re considering an injection molded part for your next project or need to replace an existing one, there are a few factors you should consider. These include design, surface finishes, tooling costs, and material compatibility. Understanding these factors can help you make the right decision. Read on to learn more about the advantages of injection molding and how to get started.
Design factors
One of the most critical design factors for injection molded parts is the wall thickness. The wall thickness affects many key characteristics of the part, from its surface finish to its structural integrity. Proper consideration of this factor can prevent costly delays due to mold issues or mold modifications. To avoid this problem, product designers must carefully consider the functional requirements of the part to determine the minimum and nominal wall thickness. In addition, they must also consider acceptable stress levels, since parts with excessively thin walls may require excessive plastic pressure and may create air traps.
Another factor to consider when designing a part is its ejection and release capabilities. If the part is released from the mold, the tools should be able to slide the plastic out. Injection molds usually have two sides, one of which is ejectable, and another that remains in the mold. In some cases, special features are required to prevent part release, such as a ramp or a gusset. These design features can increase the design flexibility, but they can also increase the cost of the mold.
When designing injection molded parts, the engineering team first determines the key design elements. These elements will make sure the injection process goes as smoothly as possible. This includes factors like wall thickness, rib design, boss design, corner transition, and weld line, among others. The engineering team will then perform a design for manufacturability analysis and, if all is well, can start building and testing the mold.
Material compatibility
Several factors can affect material compatibility of injection molded parts. When molding plastic parts, it is important to choose a material that is compatible with the part’s intended purpose. Many injection molding processes require that the two main plastic materials used are compatible with each other. This is the case in overmolding and two-shot injection molding.
The material you use to make an injection molded part will significantly impact the tolerance of the finished product. This is why material selection is as important as the design of the part. Many types of plastic resins can be used for injection molding. In addition, many of these resins can be modified or strengthened by adding additives, fillers, and stabilizers. This flexibility allows product teams to tailor the material to achieve desired performance characteristics.
One of the most common thermoplastics is polypropylene. It is extremely durable and has good impact strength and moisture resistance. This material is also recyclable and does not react with food.
Tooling costs
One of the largest costs for manufacturing injection molded parts is tooling. For an OEM, tooling costs can range from $15K per part for a simple part to $500K for a mold with complex geometry. Tooling costs vary based on the type of steel used and the production volume of the part.
To get a reasonable estimate, companies should have a final design, preliminary design, and sample part to hand when requesting quotes. The dimensions and complexity of the cavity in a mold are crucial in determining the tooling cost, as are the part tolerances. Part tolerances are based on the area covered by the part and its functions within the mold.
The type of mold you need can also impact your tooling costs. Injection molding machines can accommodate many different kinds of molds. Some molds are made from a single mold, while others require multiple molds. Some molds can be complicated, making them unmanufacturable, which in turn drives up the cost of tooling.
The costs for tooling for injection molding are not well known, but they do add up quickly. Many product development teams tend to consider the cost of the injection molding process in terms of direct materials, machine time, and labor, but that cost model often fails to take into account additional components.
Surface finishes
Surface finishes on injection molded parts are often used to mask defects, hide wear and tear, or enhance a product’s appearance. These finishes can also be useful when the product will come in contact with people’s hands. The surface texture you choose will depend on your desired functionality as well as the way you want to use the product. Generally, rougher textures provide better grip while masking minor molding imperfections. However, they can also make a product more difficult to release from the mold. This means that you may have to increase the draft angle of the mold. In order to get the best surface finish, the toolmaker and product designer must collaborate closely early in the design process.
There are several different surface finishes that can be used for injection molded parts. One type is known as the B-grade finish, and is compatible with a wide variety of injection molding plastics. Another type of finish is called a stone polishing process, and is ideal for parts that have no aesthetic value.
Overhangs
The injection moulding industry refers to overhangs on injection molded parts as “undercuts,” and these can lead to design instability. To minimize undercuts, the design must be parallel to the part’s surface. If an undercut is present, a zigzag parting line can be used.
The overhang is typically a few millimeters shorter than the surface of the mold. It is generally made from a lower-cost plastic material than the part’s surface area. The material used for the overhang should have sufficient strength to fulfill its function. An overhang will also help to prevent the piece from deforming or cracking.
Injection molding can create overhangs around the perimeter of a part. Overhangs are not always necessary; they can be added to parts as desired. Adding an overhang, however, will add substantial tooling costs. As a result, it is better to minimize the overall thickness of a design. However, in some cases an overhang can be useful to make the part look more attractive.
For parts with complex geometries, there are a few options for overhangs. Some manufacturers use side-action molds to form more complex shapes.
CNC machining
CNC machining of injection molded parts is a process that helps manufacturers achieve precise surfaces and shapes for their products. This process typically begins with the milling of the tooling, which is typically made of aluminum or steel. This tooling is then placed in a CNC mill. This machine carves the negative of the final plastic part, making it possible to achieve specific surface finishes. The process can be adapted to create a part with a complex structure or special features.
CNC machining allows the manufacturer to produce high-performance parts. This is possible because MIM parts do not experience induced stresses or internal pressure during the manufacturing process. Furthermore, the parts produced by MIM are more durable than CNC parts. Despite their advantages, CNC machining has its limitations, especially when it comes to design freedom and intricacy. This factor is largely dependent on the software used by the manufacturer or designer.
One drawback of CNC machining is its higher cost. Compared to injection molding, CNC machining is more expensive per part. The reason is that the initial mold cost is relatively high and is spread over a large number of parts. Once the injection molding process has been completed, the cost of the parts produced by this process becomes more competitive with those produced by machined parts. However, the cost gap increases with the volume of parts produced. This cost crossover generally occurs in quantities of at least 100 parts and can reach a maximum of 5000 parts.
Production volume
The production volume of injection molded parts varies depending on the material being used. Large volumes of parts are expensive to produce, while small quantities can be produced for low cost. Injection molding requires a precise mold, which is CNC-machined from tool steel or aluminum. The mold has a negative of the part that is injected, a runner system, and internal water cooling channels to aid in cooling the part. Recent advances in 3D printing materials have made it possible to produce molds for low-volume injection molding. Previously, this was not financially viable due to the high cost of traditional mold making.
A mold is used to produce plastic parts. The molding process is very fast, with each cycle taking anywhere from 30 seconds to 90 seconds. After a part is molded, it is removed from the mold and placed on a holding container or conveyor belt. Injection molded parts are generally ready for use right away and require minimal post-processing. Injection molded parts have a similar design to a photograph, since the geometry is directly transferred to the part’s surface texture.
When selecting a plastic mold, it is important to determine the volume that the part will be produced at. If the volume is low, softer plastics may be used. However, as the part is molded over, its performance characteristics may degrade. In low-volume production, it is important to consider the overall complexity of the part. This includes the part’s draft, wall thickness, and surface finish.
editor by czh 2022-12-24